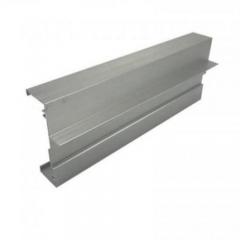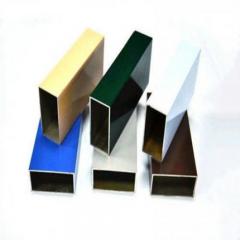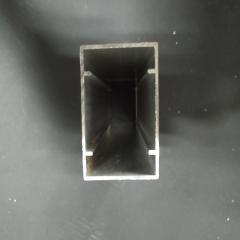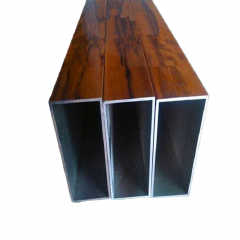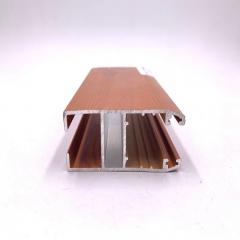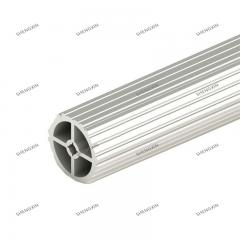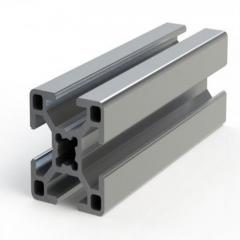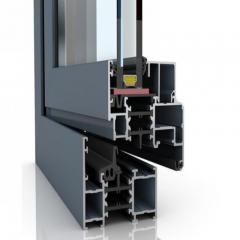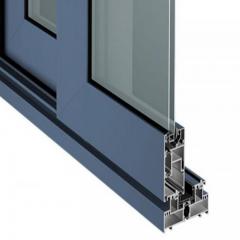
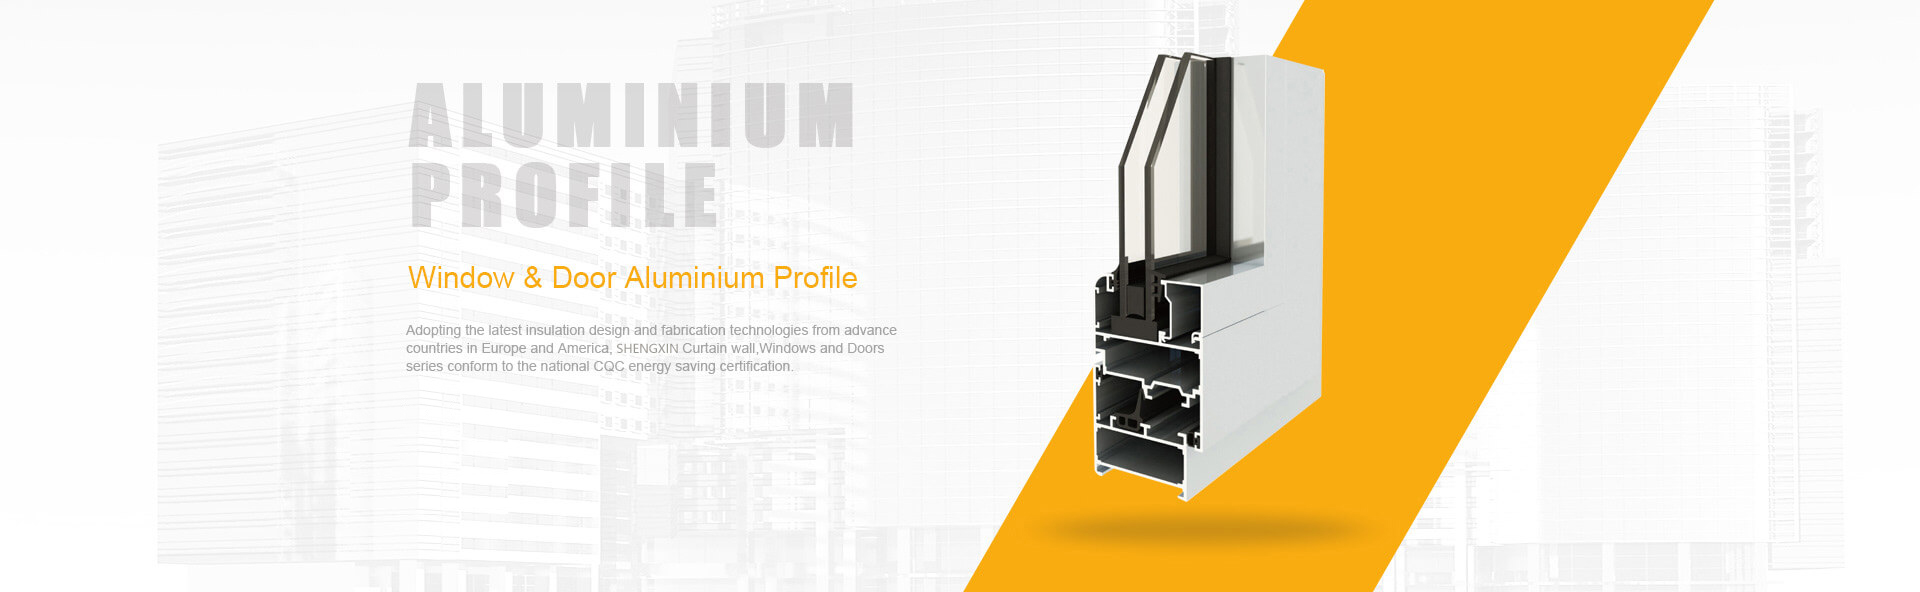
So, what is an aluminum extrusion exactly? Picture squeezing toothpaste through a shaped nozzle. The paste emerges matching the opening's form perfectly. Aluminum extrusion works the same way, just with heated metal and industrial-scale precision. This manufacturing technique forces heated aluminum alloy through a specially designed die to create consistent cross-sectional profiles. The result? Lightweight, strong components used in everything from window frames to automotive parts.
When you engage aluminum extrusion services, you're accessing a process that transforms raw aluminum billets into precisely shaped extruded profiles ready for your specific application. Whether you need simple solid bars or complex hollow sections, this versatile manufacturing method delivers repeatable accuracy across thousands of identical pieces.
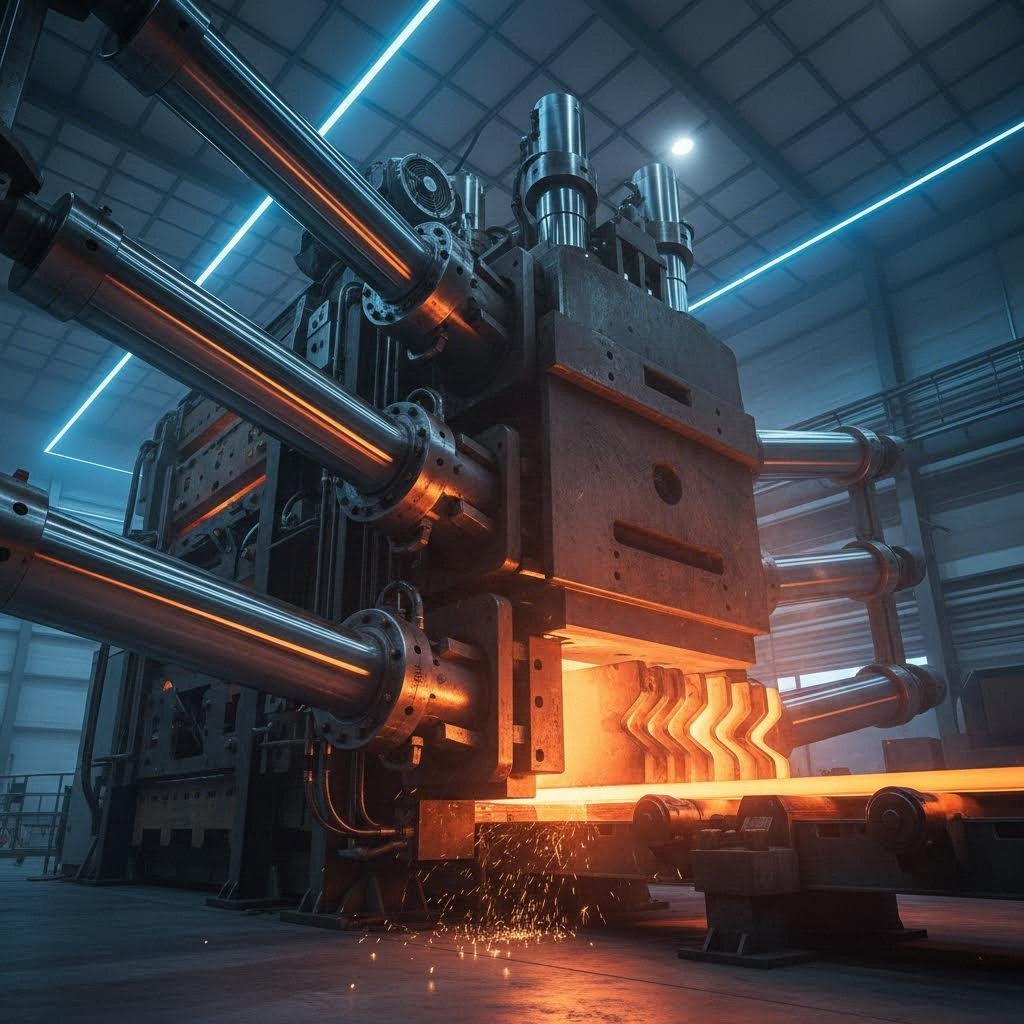
Imagine you're working with a Play-Doh Fun Factory. You select a shape, load the material, and press. Out comes a continuous form matching your chosen design. An industrial extrusion press operates on identical principles, though with considerably more sophisticated technology and temperatures reaching 800-925°F.
The force applied during extrusion is immense. Hydraulic rams can generate up to 15,000 tons of pressure, pushing malleable aluminum through die openings with incredible precision. This pressure ensures the metal completely fills every contour of the die, producing aluminum extrusion profiles with exact dimensional accuracy.
What are aluminum extrusions capable of becoming? The answer spans an impressive range. You'll find solid shapes like beams and rods, hollow tubes and channels, semi-hollow profiles with partially enclosed voids, and custom designs meeting unique specifications. Each aluminium extruded profile emerges with the same cross-section throughout its entire length, ensuring consistency across your production run.
Understanding the journey from raw material to finished product helps you communicate effectively with suppliers. Here's what happens during each critical stage:
Temperature control remains critical throughout this sequence. As Bonnell Aluminum notes, temperature is the most important factor because it determines the aluminum's final characteristics, including hardness and surface finish.
After these primary steps, extruded profiles can undergo heat treatment to enhance mechanical properties. Alloys in the 6000 series, for example, achieve optimum strength when brought to T5 or T6 tempers through controlled aging in ovens. Additional finishing operations like anodizing, powder coating, or precision machining can then transform these base profiles into finished components ready for assembly.
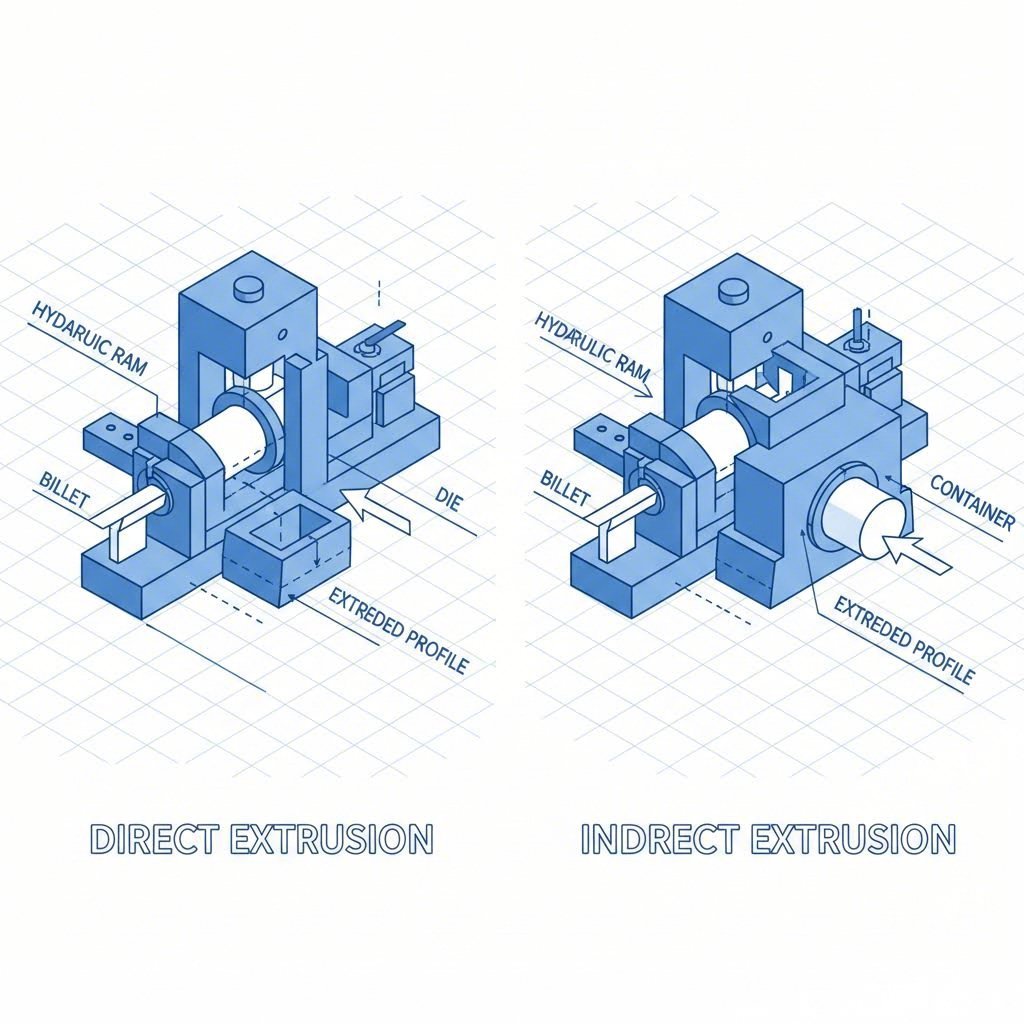
Now that you understand the basic steps, here's an important question: how does aluminum extrusion work when producing different types of profiles? The answer lies in two distinct methods—direct and indirect extrusion. Each technique shapes aluminum differently, affecting everything from surface quality to production costs. Knowing which approach suits your project helps you make smarter decisions when discussing options with suppliers.
Think of it this way. Both methods force aluminum through a die to create extrusion shapes, but the mechanics differ significantly. Your choice between them influences the final product's precision, appearance, and price point. Let's break down each approach so you can communicate confidently during your next supplier conversation.
Direct extrusion is the workhorse of the aluminum extrusion industry. In this process, a hydraulic ram pushes the heated billet through a stationary die. The material and the ram move in the same direction—hence the name "direct." Imagine pushing modeling clay through a cookie press. The force travels straight through the material, producing consistent extruded shapes on the other side.
Why do most aluminum extrusion services rely on this method? Several factors make it the go-to choice:
However, direct extrusion comes with trade-offs. As the billet moves through the container, it creates friction against the chamber walls. This friction generates heat unevenly and can cause slight inconsistencies in material flow. According to industry research, this friction also accelerates die wear, meaning more frequent tooling replacements over time.
For most standard applications—construction materials, industrial components, and general-purpose profiles—direct extrusion delivers excellent results at competitive prices. When your project prioritizes cost efficiency over ultra-fine surface finishes, this method typically makes the most sense.
Indirect extrusion flips the script. Here, the die moves toward the stationary billet rather than the other way around. The ram remains hollow, allowing the extruded profile to pass through it as the die advances. This reversed approach eliminates the friction between the billet and container walls that occurs in direct extrusion.
What does reduced friction mean for your project? You'll notice several advantages:
The catch? Indirect extrusion requires more sophisticated equipment, driving up initial costs. The process also runs slower and works best for smaller cross-sections. If you need large structural profiles quickly, this method probably isn't your best option.
Industries demanding precision—aerospace, electronics, and medical devices—often specify indirect extrusion for critical components. When surface finish and dimensional accuracy outweigh cost considerations, this technique delivers results that direct extrusion simply cannot match.
| Factor | Direct Extrusion | Indirect Extrusion |
|---|---|---|
| Surface Quality | Good—suitable for most applications | Excellent—superior finish consistency |
| Die Wear | Higher—more frequent replacement needed | Lower—extended tooling lifespan |
| Complexity Capability | Moderate—handles standard to semi-complex profiles | High—excels at intricate, thin-walled designs |
| Typical Applications | Construction, industrial parts, large sections | Aerospace, electronics, precision components |
| Relative Cost | Lower equipment and per-piece costs | Higher initial investment, slower throughput |
| Best For | High-volume, cost-sensitive projects | Precision-critical, quality-focused applications |
Here's something many buyers overlook: the extrusion press size directly determines what profiles are possible. Press tonnage—ranging from small 600-ton machines to massive 5500-ton giants—dictates the maximum profile size and complexity a supplier can produce.
Smaller presses (600T-1500T) handle lightweight, smaller cross-section profiles efficiently. They're perfect for electronics enclosures, decorative trim, and compact structural components. Larger presses (3000T-5500T) tackle heavy-duty applications like architectural curtain wall systems, large heat sinks, and substantial structural members.
When evaluating suppliers, ask about their press capabilities. A company with only smaller presses cannot produce the large profiles your construction project might require. Conversely, running small profiles on oversized equipment wastes capacity and may increase your costs.
Before requesting quotes, consider these questions for potential suppliers:
Understanding these process fundamentals transforms you from a passive buyer into an informed partner. With this knowledge in hand, you're ready to tackle the next critical decision: selecting the right aluminum alloy for your project's specific performance requirements.
You've selected your extrusion method and press size. Now comes a decision that fundamentally shapes your product's performance: which aluminum alloy should you specify? This choice affects everything from how easily your profile extrudes to how it performs years down the road. Get it right, and you'll have components perfectly matched to your application. Get it wrong, and you're stuck with parts that underperform or cost more than necessary.
Here's the reality most suppliers won't tell you upfront. Not all aluminum alloys extrude equally well. Some flow through dies like butter, producing flawless aluminium extrusion profiles with minimal effort. Others fight the process, demanding specialized equipment and expertise. Understanding these differences puts you in the driver's seat during supplier negotiations.
Think of aluminum alloys like tools in a toolbox. A hammer works great for nails but terrible for screws. Similarly, each aluminum alloy excels in specific applications while falling short in others. The key lies in matching alloy properties to your project's actual demands—not over-engineering with expensive materials or under-specifying with inadequate ones.
Five alloys dominate the aluminum extrusion landscape: 6063, 6061, 7075, 2024, and 1100. Each brings distinct advantages to the table:
According to Gabrian's aluminum alloy guide, stronger alloys with higher concentrations of alloying elements are generally more difficult to extrude and have lower extrusion rates. This directly impacts your project costs and lead times.
| Alloy | Strength Rating | Corrosion Resistance | Weldability | Typical Applications | Cost Tier |
|---|---|---|---|---|---|
| 6063 | Medium (241 MPa tensile) | Excellent | Excellent | Window frames, door frames, architectural trim, heat sinks | $ |
| 6061 | High (310 MPa tensile) | Very Good | Very Good | Structural components, trucks, marine parts, machinery | $$ |
| 7075 | Very High (572 MPa tensile) | Moderate | Poor | Aircraft structures, aerospace components, high-stress parts | $$$$ |
| 2024 | High (470 MPa tensile) | Fair | Poor | Aircraft skins, aerospace fittings, fatigue-critical parts | $$$ |
| 1100 | Low (110 MPa tensile) | Outstanding | Excellent | Chemical equipment, food processing, electrical conductors | $ |
Here's where most buyers get stuck. You need aluminum profiles for your project, but should you specify 6063 or 6061? This decision comes up constantly because these two alloys cover the vast majority of extrusion applications. Understanding their differences saves you from costly over-specification or disappointing underperformance.
6063 earns its reputation as the workhorse of aluminum extrusion shapes for good reason. Its exceptional extrudability means it flows easily through complex die geometries, producing intricate profiles with smooth surfaces. As industry experts note, 6063 readily accepts anodizing, allowing for decorative finishes that enhance both durability and aesthetics. If your project involves architectural elements, consumer products, or applications where appearance matters, 6063 delivers.
But what if your profile aluminum must bear significant loads? That's where 6061 enters the conversation. With tensile strength around 310 MPa compared to 6063's 241 MPa in T6 temper, 6061 handles structural demands that would overwhelm its lighter cousin. The trade-off? Slightly reduced extrudability and surface finish quality.
Consider these head-to-head comparisons when making your decision:
For extruded aluminium profiles destined for window systems, curtain walls, or decorative applications, 6063 makes economic and practical sense. When load-bearing capacity, structural rigidity, or demanding environmental conditions enter the picture, investing in 6061 pays dividends in long-term performance.
Armed with this knowledge, you're ready for productive conversations during the quoting process. Don't simply accept whatever alloy a supplier proposes. Instead, engage them with targeted questions that reveal whether their recommendation truly fits your needs.
Start by clearly communicating your application requirements: What loads will the profile bear? What environmental conditions will it face? How critical is surface appearance? Does the part require welding or extensive machining? These details help suppliers recommend appropriate alloys rather than defaulting to their most convenient option.
Ask suppliers to explain how their alloy recommendation affects both manufacturability and final performance. A knowledgeable partner will discuss trade-offs openly—perhaps suggesting 6063 for a complex profile shape even though 6061 offers better strength, because the manufacturing advantages outweigh the performance difference for your specific application.
Remember that alloy selection cascades through your entire project. It influences die design complexity, extrusion speed, achievable tolerances, finishing options, and ultimately your per-piece costs. Taking time to get this decision right establishes a solid foundation for everything that follows in your aluminum extrusion project.
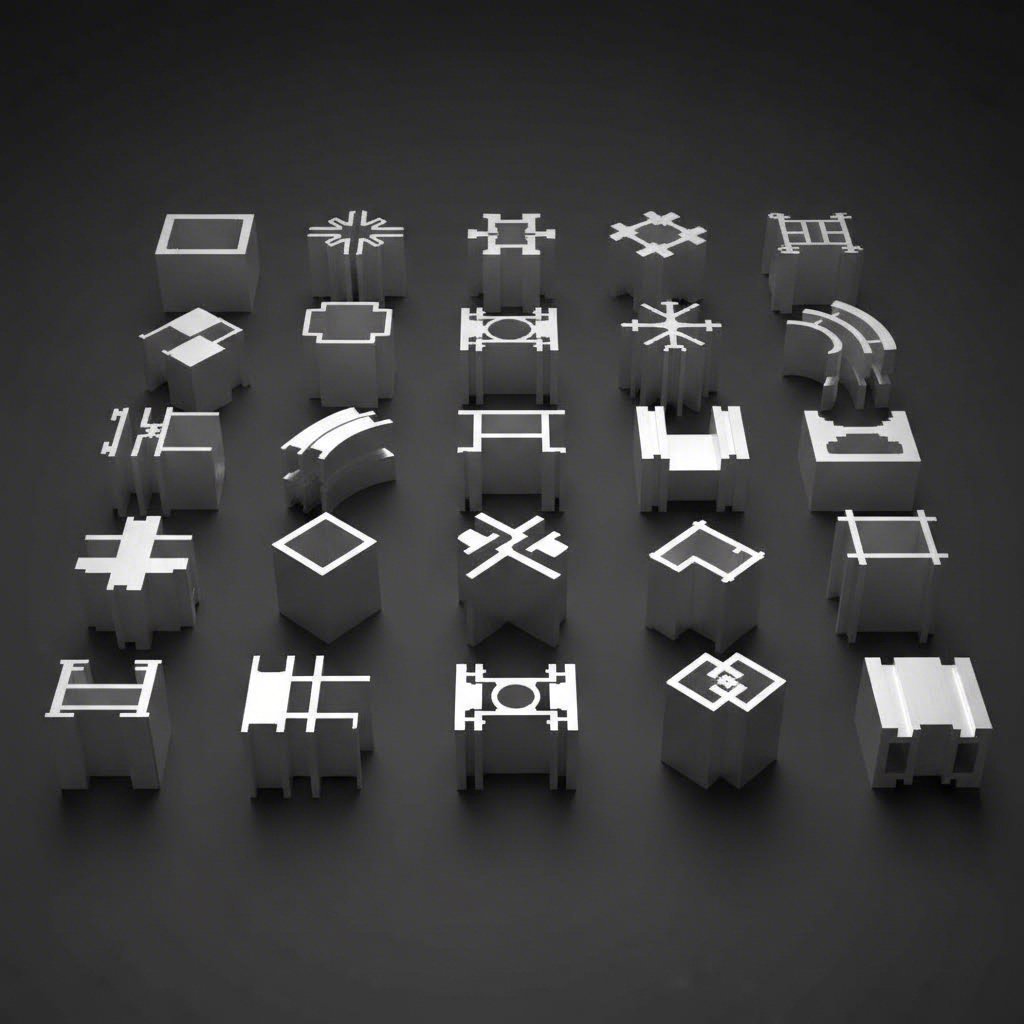
You've selected your alloy and understand the extrusion methods. Now comes a critical checkpoint many buyers skip: Is your design actually manufacturable? A brilliant concept on paper means nothing if it can't survive the extrusion process. Understanding design constraints before finalizing drawings saves you from expensive revisions, rejected quotes, and frustrating delays.
Here's what experienced engineers know: every aluminum extrusion profile must work within physical limits. Wall thickness, corner geometry, and overall complexity determine whether your custom aluminum extrusion runs smoothly or fights the process at every step. The good news? These rules aren't arbitrary restrictions—they're guidelines that help you create better, more cost-effective parts.
Think of extrusion dies like precision molds under extreme stress. Molten aluminum flows through them at high pressure, and the die must maintain its shape perfectly across thousands of cycles. Your design directly affects how well that die performs—and how long it lasts.
According to the Aluminum Extruders Council, designs are greatly enhanced when the profile's circumscribing circle diameter (CCD) stays under 8 inches and weight-per-foot remains at 3 pounds or less. These parameters significantly reduce production costs while improving quality consistency.
Here are the key design considerations that separate successful projects from problematic ones:
The Aluminum Extruders Council emphasizes these good design practices: balanced walls, minimized hollows, generous tapers, symmetrical details, strategic use of grooves and ribs, and minimized perimeter-to-cross-section ratios. Following these principles creates extruded aluminum shapes that run efficiently and cost less to produce.
Your aluminum extrusion profile doesn't just appear—it requires a custom die engineered specifically for your design. This tooling investment deserves careful consideration because die complexity directly impacts both upfront costs and ongoing production efficiency.
Simple solid profiles need straightforward flat dies. These tools cost less, wear slowly, and produce consistent results. Complex custom profile extrusions with hollow sections, thin walls, or intricate details demand multi-piece dies with internal supports, bridges, and precise flow channels. As die design experts note, flow bridges control how metal splits inside the die—if they're not right, you get thin or thick spots in your finished profile.
Die material selection also matters significantly. Standard H13 steel handles general applications well, while high-wear situations may require D2 steel or even carbide inserts. Surface treatments like nitriding extend die life, reducing your long-term tooling costs.
Before finalizing your design, consider these die-related factors:
Even experienced designers stumble into traps that complicate manufacturing. Here are the mistakes that cause the most headaches—and how to sidestep them:
Ignoring Circumscribing Circle Limits: Most economical aluminum extruded shapes fit within a 1-10 inch CCD. Profiles exceeding 12 inches require specialized presses that fewer suppliers operate. As the Aluminum Extruders Council notes, profiles below 8 inches CCD reduce costs significantly.
Specifying Unnecessary Tight Tolerances: Standard extrusion tolerances satisfy most applications. Demanding tighter specs increases die complexity, slows production, and may require secondary machining—all adding cost without functional benefit.
Creating Extreme Wall Thickness Variations: A profile with 1mm walls next to 10mm sections creates cooling nightmares. The thick areas cool slower than thin ones, causing warping and internal stresses. Keep thickness ratios below 3:1 when possible.
Designing Unsupported Projections: Long, thin fins without adequate support flex during extrusion. Either add connecting webs or redesign to reduce projection length.
Overlooking Draft Angles: Slight tapers help profiles release cleanly from dies. Zero-draft designs may work but increase die wear and risk surface scratching.
Here's an honest reality check: aluminum extrusion isn't always the best manufacturing choice. Recognizing when alternative processes make more sense saves you from forcing a square peg into a round hole.
According to manufacturing process comparisons, the optimal choice depends on application requirements, production volume, and specific performance needs. Consider these scenarios where other methods outperform extrusion:
Choose CNC Machining When:
Choose Die Casting When:
Choose Roll Forming When:
Custom aluminum products destined for prototyping often make more sense as CNC-machined parts initially, with extrusion dies developed only after design validation.
The smartest approach to design optimization? Engage your extrusion supplier's engineering team early—before drawings reach "final" status. Experienced suppliers have seen thousands of profiles and know instantly which designs will run smoothly and which will struggle.
During the design phase, ask suppliers to review your concepts and suggest improvements. They can identify potential problems with wall thickness transitions, recommend optimal corner radii, and propose modifications that maintain functionality while improving extrudability. This collaboration often reduces die costs by 20-30% while improving part quality.
Come prepared with clear information about your application requirements: loads, environmental exposure, finishing needs, assembly constraints, and target costs. The more context you provide, the better guidance you'll receive.
Remember that minor design tweaks can yield significant manufacturing benefits. A slightly larger corner radius, an added support rib, or a modest wall thickness increase might transform a difficult extrusion into an efficient one. Your supplier's engineering team represents a valuable resource—use their expertise to optimize your custom aluminum extrusions before committing to production tooling.
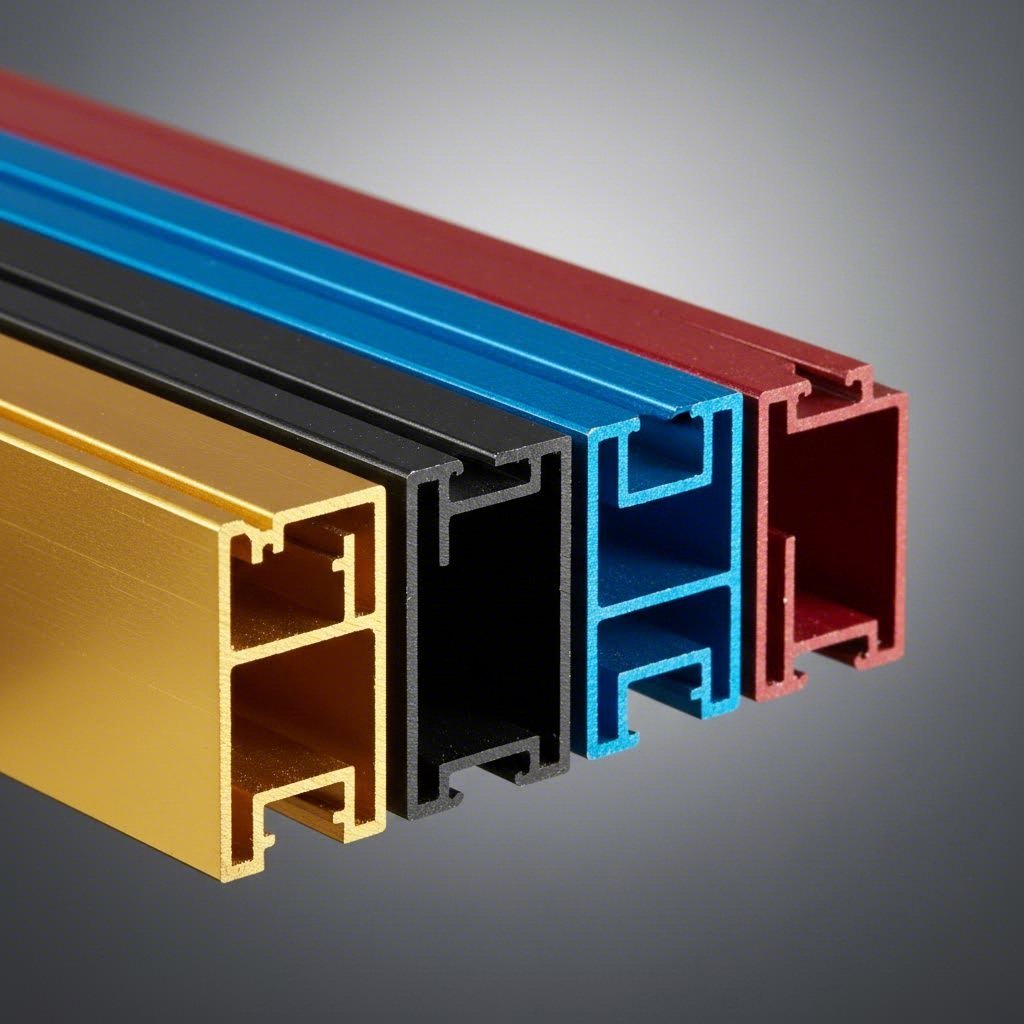
Your aluminum profile just emerged from the extrusion press. It has the right shape and alloy—but is it ready for your application? In most cases, the answer is no. Raw extrusions arrive with mill finishes that offer minimal protection and unremarkable appearance. This is where secondary operations transform basic profiles into finished components ready for demanding real-world use.
Think of secondary operations as the final tailoring of a suit. The fabric and cut matter, but proper finishing elevates everything. Surface treatments add durability and visual appeal. Aluminum extrusion machining creates precise features impossible to achieve during extrusion alone. Together, these processes bridge the gap between raw material and functional product.
Why do surface finishes matter so much? According to Gabrian's finishing guide, the right surface finish can elevate products from "good" to "outstanding"—improving corrosion resistance, wear resistance, and aesthetic appearance to make extrusions last longer and look better.
Each finishing method brings unique advantages to your project. Understanding these differences helps you specify the right treatment for your specific application requirements.
Anodizing stands apart from other finishes because it doesn't apply an external coating. Instead, an electrochemical process stimulates the naturally-occurring aluminum oxide layer to grow thicker. This integrated protection resists wear and corrosion exceptionally well. As A-Line Automation notes, anodizing is highly resistant to wear and tear, making it a great choice for outdoor applications. Standard anodizing produces clear, bronze, or black finishes, while custom colors like champagne, rose gold, and architectural bronze require specialized dye processes.
Powder coating delivers the widest color palette with excellent durability. The process sprays dry paint powder electrostatically onto cleaned aluminum surfaces, then bakes it to create a tough, even finish. You'll find powder-coated aluminium extrusion trim on everything from window frames to industrial equipment. While not as hard as anodized surfaces, powder coating provides exceptional appearance and corrosion protection when the coating remains intact.
PVDF coatings excel in demanding exterior applications. These resin-based finishes resist fading, chemicals, and harsh weather conditions better than most alternatives. Architectural projects like aluminum wall cladding frequently specify PVDF for its long-term color stability. Unlike powder coating, PVDF doesn't require oven curing and applies in thinner layers.
Micro-arc oxidation (MAO) represents the cutting edge of surface treatment technology. This advanced process creates ceramic-like coatings with exceptional hardness and wear resistance—ideal for components facing extreme conditions.
| Finish Type | Durability Rating | Color Options | Cost Tier | Best Applications |
|---|---|---|---|---|
| Anodizing (Standard) | Excellent—integrated protection | Clear, bronze, black | $$ | Architectural elements, industrial components, outdoor fixtures |
| Anodizing (Custom Colors) | Excellent | Champagne, rose gold, custom hues | $$$ | Premium architectural features, decorative applications |
| Powder Coating | Very Good—intact coating required | Virtually unlimited RAL colors | $$ | Consumer products, furniture, extruded aluminum trim |
| PVDF Coating | Outstanding fade/chemical resistance | Wide matte color range | $$$ | Exterior cladding, curtain walls, marine environments |
| Micro-arc Oxidation | Superior—ceramic-like hardness | Limited (gray, black) | $$$$ | High-wear components, extreme environment parts |
Extrusion creates your profile's cross-section, but what about holes, threads, slots, and other features? That's where aluminium extrusion machining enters the picture. As industry experts explain, machining transforms an extruded profile into a functional component by adding precise features—holes, threads, grooves, flat surfaces—ensuring alignment, assembly fit, and performance under service conditions.
CNC machining capabilities extend far beyond simple cuts. Modern extrusion machining centers handle:
Coolant plays a critical role during machining operations. Although aluminum cuts more easily than steel, the process still generates significant heat. Proper cooling maintains dimensional accuracy, prevents part distortion, and extends tool life—all factors affecting your final part quality and cost.
Here's what many buyers overlook: every secondary operation adds time and expense to your project. A simple extruded profile might ship in two weeks, but adding anodizing extends that timeline. Specify custom powder coating colors, precision machining, and assembly services? You're looking at significantly longer lead times.
Planning for these additions upfront prevents schedule surprises:
Costs follow similar patterns. Each operation requires setup, labor, and quality inspection. High-volume orders spread fixed costs across more pieces, reducing per-unit pricing. Low-volume projects bear these costs more heavily.
Imagine coordinating separate vendors for extrusion, anodizing, machining, and assembly. Each handoff introduces delays, shipping costs, and quality risks. Now picture a single supplier handling everything under one roof.
Integrated aluminum extrusion services providers like Shengxin Aluminium consolidate these operations, offering comprehensive capabilities from die development through finished components. With 35 extrusion presses ranging from 600T to 5500T, plus state-of-the-art CNC machining centers and in-house finishing facilities, they handle complete projects without external coordination headaches.
Their surface treatment options span the full spectrum: standard and custom-color anodizing (including champagne and rose gold), powder coating, PVDF, and micro-arc oxidation for demanding applications. When your project requires precise cutting, drilling, bending, or curved aluminum extrusion forming, their machining capabilities deliver without shipping parts to outside vendors.
This integration translates to faster turnarounds, lower total costs, and simplified project management. One point of contact, one quality system, one responsibility for your finished parts. For complex projects requiring multiple operations, this approach dramatically reduces the coordination burden while improving overall quality control.
With your finishing and fabrication options clearly defined, the next critical question becomes: what will all this actually cost? Understanding the factors that drive aluminum extrusion pricing helps you budget accurately and negotiate effectively with suppliers.
You've designed your profile, selected an alloy, and specified your finishing requirements. Now comes the question that determines project feasibility: how much will this actually cost? Unlike commodities with transparent pricing, aluminum extrusion projects involve multiple cost components that interact in complex ways. Understanding these factors transforms you from a passive quote recipient into an informed negotiator.
Here's the reality: pricing for these services isn't arbitrary. Every dollar traces back to specific inputs—materials, tooling, labor, and processing. When you understand what drives costs, you can make smarter design decisions, negotiate more effectively, and avoid budget surprises that derail projects.
Think of your extrusion project as four distinct cost buckets. Each one contributes to your final price, and each responds to different levers you can pull during the design and procurement process.
Die and Tooling Costs (One-Time Investment)
Every custom extrusion requires a die machined specifically for your profile. According to Gabrian International, tool costs for standard architectural and industrial applications typically range from $400 to $1,000. Large parts requiring 2,000-4,000 ton presses can push die costs as high as $2,000. Complex or multi-hollow dies may reach $5,000 or more.
The good news? Many manufacturers refund tooling costs if you purchase a stipulated amount within two years. Most also cover replacement dies at no charge once your original tooling wears out—provided orders continue. Normal die turnaround runs 3-4 weeks, with production following within a week of sample approval.
Material Costs (Variable)
Raw aluminum represents your largest variable expense. The London Metal Exchange sets baseline pricing that has fluctuated dramatically—anywhere from $1,500 to $3,500 per metric ton in recent years. Geopolitical events, environmental regulations, and global demand all influence these swings.
Different alloy grades carry different premiums. Standard 6063 costs less than structural 6061, while aerospace-grade 7075 commands significant price increases. When wondering where to buy aluminum extrusion at competitive rates, consider suppliers who can lock in material pricing for ongoing production needs.
Extrusion Run Costs (Per-Unit)
This covers the actual manufacturing: press time, labor, energy, and overhead. Regional labor rates significantly impact this component—Asian manufacturing typically offers lower costs than North American or European production, though logistics add complexity.
Secondary Operation Costs (Per-Unit)
As industry data indicates, anodizing and powder coating run $1,200 to $1,400 per metric ton depending on profile complexity. Specialized finishes like wood-grain effects cost significantly more. Simple drilling operations add $200-$300 per metric ton, while complex CNC machining can range from $900 to $2,100 per ton.
Several factors push costs higher across all these categories:
Before investing in custom extrusion aluminum, ask yourself: does a standard profile already exist that meets my needs? With over 10,000 standard aluminum profiles available from various suppliers, the answer is often yes.
According to industry analysis, standard aluminum profiles typically cost 30% to 50% less than custom alternatives. This gap exists because standard profiles eliminate die development costs entirely, benefit from mass-production efficiencies, and ship from existing inventory.
When do custom extrusions make economic sense despite higher initial costs?
The break-even point varies by project. A profile extrusion company producing 10,000 meters of custom extrusion absorbs die costs much more effectively than one ordering 500 meters. At high volumes, custom profiles often deliver better total value through optimized designs and reduced assembly complexity.
Every aluminum extrusion company sets minimum order quantities (MOQs) that affect project viability. These minimums exist because press setup, die installation, and quality verification consume time regardless of run length. Spreading these fixed costs across too few pieces makes production economically unworkable.
Typical MOQ structures look like this:
For prototype or low-volume needs, consider these strategies: source standard profiles and modify them through machining, work with suppliers offering prototype-friendly terms, or explore distributors specializing in small-quantity custom extrusions at higher per-piece rates.
Requesting quotes without proper preparation wastes everyone's time and produces unreliable estimates. Aluminum extrusion companies need specific information to price your project accurately.
Come prepared with:
The more complete your RFQ package, the more accurate your quotes will be. Vague requests generate padded estimates as suppliers protect themselves against undefined scope. Detailed specifications enable competitive pricing based on actual project requirements.
With cost factors clearly understood, your next consideration becomes timing. How long will your project actually take from quote approval to delivered parts? Understanding realistic lead times prevents schedule disasters and helps you plan production effectively.
You've got your design finalized, costs estimated, and supplier selected. Now the question everyone asks: when will my parts actually arrive? Aluminum extrusion services timelines often surprise buyers accustomed to quick-turnaround manufacturing. Understanding realistic lead times prevents schedule disasters and helps you plan production milestones effectively.
Here's what many buyers discover too late: custom aluminum extrusion parts don't materialize overnight. Each project phase—from die fabrication through final delivery—requires specific time allocations that compound into total lead times spanning weeks or months. Knowing these timeframes upfront lets you work backward from your deadlines to determine when supplier engagement must begin.
Every aluminum extrusion project moves through distinct phases, each with its own timeline requirements. According to Profile Precision Extrusions, lead time consists of three primary factors: tooling lead time, extrusion lead time, and fabrication lead time. Understanding each component helps you set accurate expectations.
Tooling Lead Time varies by die complexity. Simple solid dies for basic shapes like rods or angles take 2-3 weeks to manufacture. Hollow profiles requiring multi-piece dies with mandrels extend this to 3-4 weeks. Complex custom dies with intricate geometries may require 4-6 weeks for proper engineering and fabrication.
Extrusion Lead Time includes both queue waiting and actual production. Here's a reality check: approximately 75% of extrusion lead time involves waiting in the production queue, not actual pressing. The physical extrusion itself may take only 15 minutes to a few hours depending on order size. After extrusion, profiles require cooling, stretching, cutting, and artificial aging—adding roughly 48 hours before parts are ready for the next phase.
Fabrication Lead Time depends on your secondary operation requirements. Each process—cutting, deburring, drilling, anodizing—typically adds 1-2 weeks to your timeline.
| Project Phase | Standard Timeline | Rush Timeline | Key Variables |
|---|---|---|---|
| Die Design & Fabrication | 2-6 weeks | 1-3 weeks | Profile complexity, hollow vs solid, supplier capacity |
| Sample Production | 1-2 weeks | 3-5 days | Approval speed, revision requirements |
| Production Run | 2-4 weeks | 1-2 weeks | Order volume, press availability, profile size |
| Finishing Operations | 1-3 weeks | 3-7 days | Treatment type, custom colors, multiple processes |
| Shipping (Domestic) | 3-7 days | 1-2 days | Distance, freight method, packaging requirements |
| Shipping (International) | 2-6 weeks | 1-2 weeks | Origin/destination, customs, shipping method |
For a practical example: a custom extruded tube requiring cutting, deburring, and black anodizing would typically follow this timeline: extrusion (4 weeks) + cutting (1 week) + deburring (1 week) + anodizing (1 week) = 7 weeks total, as industry sources confirm.
Why do some projects ship in four weeks while similar ones take twelve? Several variables dramatically influence your aluminum extrusion supply timeline.
Order Volume affects scheduling priority and production efficiency. Large orders justify dedicated press time and streamlined handling. Smaller quantities may wait for consolidation with similar profiles or alloys, extending queue times. However, massive orders requiring multiple press runs naturally take longer to complete.
Profile Complexity impacts every phase. Intricate aluminium extrusion parts with tight tolerances require more careful die development, slower extrusion speeds, and additional quality verification. Simple solid shapes move through production far faster than complex hollow sections.
Finishing Requirements compound quickly. Standard clear anodizing adds less time than custom-color processes. Specifying multiple treatments—say, anodizing by precision machining—creates sequential operations that extend timelines significantly.
Prototype Runs vs Production Orders operate on different timelines. Prototype aluminum extrusions typically receive expedited handling since they're proving out new designs. Quantities are small, and suppliers understand the urgency of getting samples for validation. Production orders follow more standard scheduling, though established die availability accelerates the process.
Stock aluminum extrusions offer the fastest path to parts. Standard profiles ship from inventory within days rather than weeks. When your application can use off-the-shelf shapes, bypassing custom die development eliminates the longest lead time component entirely.
Need parts faster than standard timelines allow? Rush capabilities exist, but they come with trade-offs you should understand upfront.
Expedited production typically costs 15-30% more than standard scheduling. You're paying for priority queue positioning, overtime labor, and disruption to other customers' orders. Some suppliers offer tiered rush options: moderate acceleration at modest premiums, or maximum speed at significant cost increases.
Be realistic about what rushing can achieve. Die fabrication has physical limits—tool steel must be machined precisely regardless of urgency. Artificial aging requires specific time at temperature. Anodizing baths need adequate dwell time. Cutting corners on these processes compromises quality.
When requesting rush delivery, ask suppliers specifically: "What timeline is achievable, and what are the cost implications?" rather than simply demanding faster delivery. Experienced suppliers will identify which phases can compress and which cannot.
Smart project planning means engaging suppliers well before you need parts. Work backward from your production deadline to establish when each phase must complete.
For custom aluminum extrusion services, engage suppliers during the design phase—not after drawings are finalized. Early involvement allows engineering teams to suggest modifications that improve manufacturability and potentially reduce lead times. It also reserves your spot in production queues before capacity fills.
These practices help avoid common delays:
According to manufacturing experts, effective communication and collaboration between all stakeholders are essential for a streamlined production process. Regular updates and feedback help keep projects on track.
With realistic timeline expectations established, you're ready to evaluate potential suppliers. But how do you distinguish excellent partners from problematic ones? The right evaluation criteria separate suppliers who deliver reliably from those who create headaches throughout your project.
You've defined your project requirements, understood costs, and mapped out timelines. Now comes arguably the most consequential decision: which supplier gets your business? The wrong choice leads to missed deadlines, quality failures, and frustrating communication breakdowns. The right partner delivers consistent results while making your job easier. How do you tell them apart before signing a purchase order?
Here's what separates successful sourcing from costly mistakes: systematic evaluation based on criteria that actually predict performance. Too many buyers focus solely on quoted prices, ignoring factors that determine whether those attractive numbers translate into real-world satisfaction. Custom aluminum extruders vary dramatically in capabilities, quality systems, and customer support. Understanding what to look for—and what to avoid—protects your project from preventable problems.
Walking into supplier discussions without a structured evaluation framework puts you at a disadvantage. These criteria separate profile precision extrusions providers who deliver reliably from those who overpromise and underperform.
A supplier's press fleet directly determines what profiles they can produce—and how efficiently. According to industry experts, small presses (600-1800T) handle thin and precise profiles, medium presses (2000-3500T) suit general industrial applications, and large presses (5000-10,000T) produce heavy structural components.
Why does this matter for your project? A profile custom extrusion company with only small presses cannot manufacture your large architectural sections. Conversely, running small profiles on oversized equipment wastes capacity and may inflate your costs. Ask specifically: "What press sizes do you operate, and which would you recommend for my profile?"
Suppliers with multiple press capacities offer flexibility when production volumes change or when you need varied profile sizes across different projects. This range indicates a mature operation capable of handling diverse requirements.
Certifications aren't just wall decorations—they represent documented commitments to process control and consistent quality. Here's what key certifications signal about a supplier's capabilities:
Military and defense supplier credentials deserve special attention. These qualifications indicate exceptionally rigorous quality systems because defense contracts demand zero-defect performance with complete traceability. A supplier meeting military specifications has proven their ability to maintain consistent quality under demanding scrutiny—confidence that transfers to your commercial projects.
Can you reach knowledgeable engineers when design questions arise? Custom aluminum extrusions suppliers with strong technical teams provide Design for Manufacturability (DFM) feedback, catching potential problems before they become expensive mistakes. According to procurement specialists, capable suppliers proactively prevent issues instead of reacting after defects occur.
Ask about engineering support during these critical phases:
Where do secondary operations happen? Suppliers handling anodizing, powder coating, and machining under one roof maintain better quality control and faster turnarounds than those shipping parts to subcontractors. As industry sources confirm, integration reduces transportation between subcontractors, prevents damage, and shortens lead time.
For example, Shengxin Aluminium maintains 35 extrusion presses ranging from 600T to 5500T alongside state-of-the-art CNC machining centers and comprehensive finishing facilities. Their in-house capabilities span anodizing in custom colors like champagne and rose gold, powder coating, PVDF, and micro-arc oxidation. This integration means your custom extruded aluminum moves from die development through finished parts without leaving their quality system.
How quickly do potential suppliers respond to your inquiries? Initial communication speed often predicts ongoing responsiveness throughout your project. Experienced profile custom extrusions providers understand that clear, proactive communication prevents misunderstandings and delays.
Evaluate whether suppliers:
Some warning signs appear early in the evaluation process. Recognizing them saves you from partnerships destined for frustration.
Vague Answers to Technical Questions: When suppliers can't clearly explain their processes, tolerances, or capabilities, they likely lack the expertise to handle complex projects. Knowledgeable aluminum extrusion suppliers speak confidently about their equipment specifications and quality systems.
Reluctance to Provide References: Established suppliers have satisfied customers willing to share their experiences. Hesitation suggests either limited experience or problematic track records.
Outsourced Die Manufacturing: According to industry analysis, many suppliers outsource die manufacturing to third parties, leading to longer lead times and slower problem resolution. If the die fails or produces inaccurate dimensions, delays ripple across the entire project. In-house die capability indicates operational maturity and faster response when issues arise.
No Quality Documentation: Professional suppliers provide traceable lot data and QA certificates with each batch. Inability or unwillingness to furnish this documentation suggests inadequate quality systems.
Unrealistic Timeline Promises: Suppliers promising delivery faster than industry norms either cut corners or tell you what you want to hear. Both scenarios end badly.
Price Significantly Below Competitors: Extremely low quotes often mean hidden costs, quality compromises, or bait-and-switch tactics. Sustainable businesses price fairly—dramatic underpricing warrants skepticism.
Don't rely solely on what suppliers tell you. Verify their capabilities through concrete evidence.
Request Samples: Actual production samples reveal surface quality, dimensional accuracy, and finishing consistency better than any specification sheet. Examine samples critically—measure dimensions, inspect surfaces, and test finishes.
Review Facilities: Factory visits (virtual or in-person) confirm equipment claims and organizational discipline. Well-maintained facilities with organized workflows suggest operational competence. Chaos and clutter often predict quality problems.
Check References: Contact current customers with similar project requirements. Ask specifically about on-time delivery, quality consistency, and problem resolution. References from your industry carry extra weight since they understand your specific challenges.
Verify Certifications: Request copies of current certificates and confirm validity with issuing bodies if necessary. Certifications with expired dates or from unknown registrars warrant investigation.
The most valuable supplier relationships extend beyond transactional part production. Comprehensive partners support your project from initial concept through ongoing production—providing technical guidance during design, efficient die development, consistent manufacturing, and responsive service when questions arise.
With over 30 years of industry experience, Shengxin Aluminium exemplifies this end-to-end approach. Their technical team provides support from die development through mass production, ensuring designs optimize for manufacturability while meeting your performance requirements. Factory-direct pricing eliminates intermediary markups, delivering value without sacrificing capability.
When evaluating potential partners, assess their willingness and ability to engage throughout your project lifecycle. Suppliers invested in your success—not just your purchase order—become genuine assets to your manufacturing operations.
Armed with these evaluation criteria, you can distinguish exceptional aluminum extrusion suppliers from merely adequate ones. But supplier capability only matters if it matches your application requirements. Understanding how different industries leverage extrusion helps you communicate your specific needs effectively during the selection process.
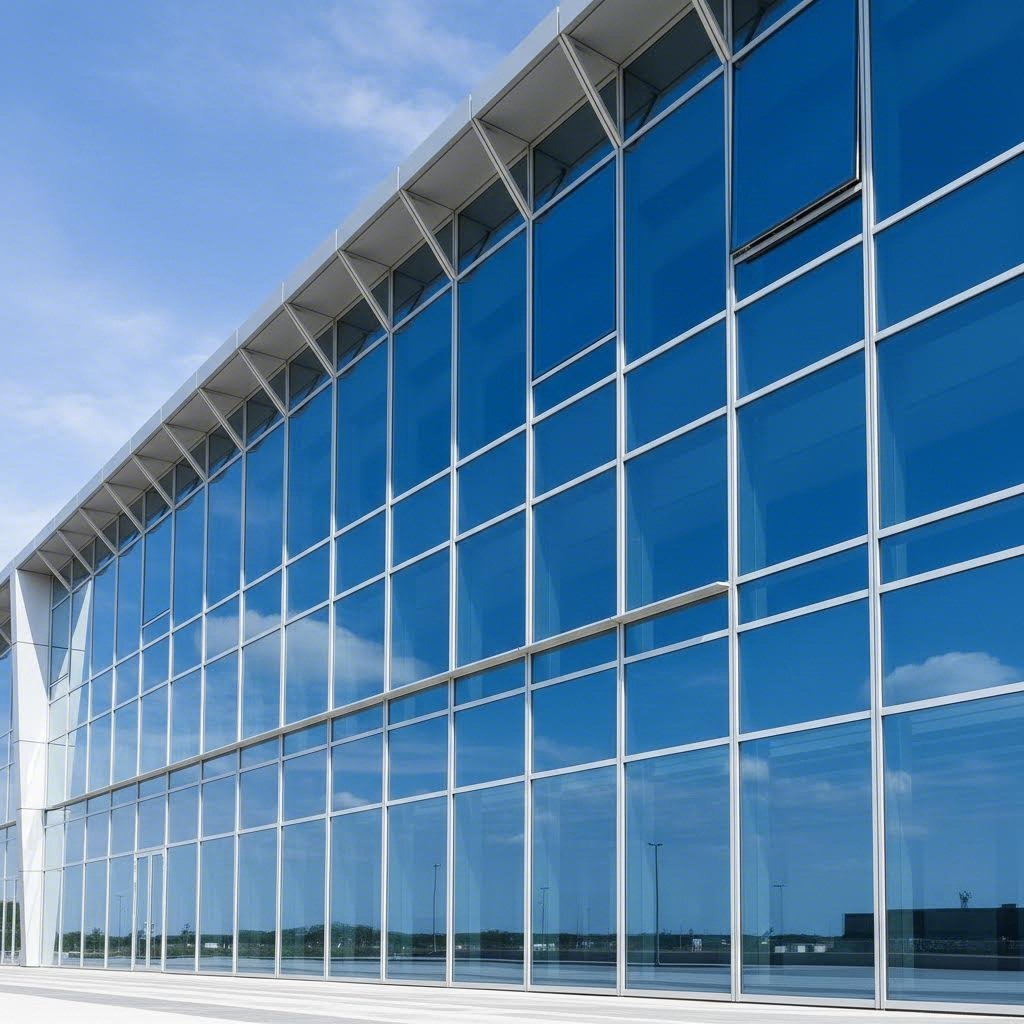
So, what are aluminum extrusions used for in the real world? The answer spans virtually every industry you can imagine. According to the Aluminum Extruders Council, extrusions are everywhere—at home in windows, doors, railings, and appliances; on the road, water, and in the air; at work, school, gyms, playgrounds, stadiums, and supermarkets. This versatility stems from aluminum's unique combination of strength, light weight, corrosion resistance, and design flexibility.
Here's what makes aluminum profile extrusion so widely adopted: each industry leverages different properties for different purposes. Construction prioritizes structural integrity and weather resistance. Electronics demands thermal conductivity. Transportation values weight reduction. Understanding these sector-specific requirements helps you communicate effectively with suppliers and ensures your extrusion profiles match your application's actual demands.
Walk into any modern building and you're surrounded by aluminium extrusion applications. Window frames, door systems, curtain walls, storefronts, and structural framing all rely on extruded aluminum's ability to combine strength with design flexibility. The construction industry represents the largest market for extrusion profiles, consuming roughly 40% of all aluminum extrusions produced.
Why does architecture favor these profiles so heavily? Aluminum delivers the structural performance of heavier materials at a fraction of the weight. This reduces foundation requirements, simplifies installation, and enables larger glass expanses in modern designs. Additionally, excellent corrosion resistance means facades maintain their appearance for decades with minimal maintenance.
Typical applications and key considerations for construction include:
When specifying architectural extrusions, communicate your project's exposure conditions clearly. Coastal environments demand enhanced corrosion protection. High-traffic areas require durable finishes resistant to scratching. Energy codes may dictate thermal performance requirements that affect profile design.
Step onto a manufacturing floor and you'll find extrusion profiles forming the backbone of modern production. Machine frames, conveyor systems, equipment housings, and safety guarding all leverage aluminum's combination of strength, light weight, and easy fabrication. Unlike architectural applications focused on appearance, industrial uses prioritize function and durability.
According to Gabrian International, aluminum extrusions play an important role in the electronics industry specifically because good thermal conductivity properties make them well-suited to heat dissipation applications. Extrusion is one of the most common methods of heatsink manufacturing, transforming aluminum's natural thermal properties into functional cooling solutions.
Industrial applications and their specific requirements include:
Electronics applications present unique considerations:
When sourcing industrial extrusions, specify your operating environment clearly. Temperature extremes, chemical exposure, and vibration all affect material and finish selection. Electronics applications may require specific alloy certifications or RoHS compliance documentation.
Transportation represents one of the most demanding environments for extrusion profiles. Weight reduction directly improves fuel efficiency and performance, making aluminum's strength-to-weight ratio invaluable. From passenger vehicles to rail cars, aircraft to marine vessels, extruded components reduce mass while maintaining structural integrity.
Key transportation applications include:
Specialty applications extend into medical equipment, sporting goods, renewable energy, and consumer products. Each sector brings unique requirements—biocompatibility for medical devices, aesthetic excellence for consumer goods, UV resistance for solar installations.
Your supplier can only meet your needs if they understand them. When requesting quotes, provide context beyond basic dimensions and quantities. Explain your application, operating environment, and performance expectations.
Consider sharing these details during the quoting process:
Experienced suppliers recognize that different industries operate under different rules. Construction projects follow building codes. Automotive components meet OEM specifications. Aircraft aluminum extrusions require FAA-traceable documentation. By clearly communicating your industry context, you enable suppliers to provide appropriate recommendations rather than generic solutions.
The most productive supplier relationships develop when both parties understand not just what you need, but why you need it. This context helps engineering teams optimize designs for your specific application while avoiding over-specification that drives unnecessary costs. Whether you need small aluminum extrusions for electronics cooling or massive structural sections for architectural facades, clear communication of industry requirements ensures your project succeeds.
Custom aluminum extrusion costs depend on four main components: die tooling ($400-$5,000 one-time), raw material ($1,500-$3,500 per metric ton based on LME pricing), extrusion run costs, and secondary operations. Anodizing and powder coating add $1,200-$1,400 per metric ton, while CNC machining ranges from $200-$2,100 per ton depending on complexity. Many suppliers refund tooling costs if you purchase stipulated amounts within two years. Standard profiles cost 30-50% less than custom alternatives since they eliminate die development.
6063 aluminum is the most common extrusion alloy, offering excellent extrudability, superior surface finish, and easy anodizing—ideal for architectural applications like window frames. 6061 provides approximately 29% higher yield strength (276 MPa vs 214 MPa) and better structural performance for load-bearing applications. 6063 conducts heat better (200 W/m-K vs 170 W/m-K), making it preferred for heat sinks, while 6061 suits machinery, trucks, and structural components requiring higher mechanical performance.
Custom aluminum extrusion lead times typically span 7-12 weeks total. Die fabrication takes 2-6 weeks depending on complexity, sample production adds 1-2 weeks, production runs require 2-4 weeks, and finishing operations add 1-3 weeks. International shipping extends timelines by 2-6 weeks. Approximately 75% of extrusion lead time involves queue waiting rather than actual production. Rush orders can compress timelines by 30-50% at 15-30% premium pricing.
Essential certifications include ISO 9001:2015 for baseline quality management with documented processes and regular audits. IATF 16949 applies to automotive suppliers, while AS9100 covers aerospace requirements including safety and traceability. EN755-9 and EN12020-2 demonstrate precision manufacturing to European dimensional standards. RoHS and REACH compliance addresses environmental and materials safety. Military/defense credentials indicate exceptionally rigorous quality systems suitable for demanding commercial applications.
Aluminum extrusions serve diverse industries. Construction consumes roughly 40% for window frames, curtain walls, and structural framing using 6063 alloy. Industrial applications include machine frames, conveyor systems, and T-slot modular assemblies. Electronics rely on extruded heat sinks and enclosures for thermal management. Transportation uses high-strength alloys for automotive crash structures, rail components, and aircraft parts. Architectural trim, LED lighting profiles, and solar panel frames represent growing specialty applications.


 Servicio en línea
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 español
 English
 français
 Deutsch
 русский
 português
 العربية
 ไทย
 Việt
 Українська