Have you ever wondered how architects create those sweeping curved facades or how automotive engineers craft lightweight yet sturdy vehicle frames? The answer often lies in bending aluminum extrusions—a process that transforms straight profiles into graceful curves while preserving structural strength.
At its core, bending aluminum extrusions involves applying controlled force to reshape extruded profiles into curved or complex forms. Unlike cutting and welding multiple pieces together, this method uses a single continuous profile, reducing material waste and maintaining the aluminum's inherent integrity. The process subjects the workpiece to tension, compression, and sometimes torsion simultaneously, requiring precise control to achieve quality results.
Aluminum stands apart from other metals thanks to its exceptional combination of properties. Compared to steel, aluminum is significantly more malleable and elastic, allowing it to bend without cracking or losing structural integrity. This ductility means you can form intricate shapes that would cause harder metals to fail.
Unlike steel, which tends to crack or deform when bent beyond its limits, aluminum's high ductility allows it to be shaped into curves and complex forms while maintaining its structural integrity—making it the preferred choice for applications demanding both design flexibility and durability.
The secret lies in aluminum's crystalline structure and the alloy composition you select. Different alloys from the 6XXX series, for instance, offer varying degrees of bendability based on their chemical makeup and temper treatment. This flexibility in material selection gives engineers remarkable control over the final product's characteristics.
The demand for curved aluminum extrusion continues to surge across multiple industries. Consider these key applications:
Modern bending technology has evolved dramatically—where manufacturers once required minimum material thicknesses of 3.0 millimeters, today's processes can handle materials as thin as 1.0 millimeter. This advancement opens doors for lightweight designs that were previously impossible.
Throughout this guide, you'll discover the six primary methods for bending aluminum, learn how to select the right alloy for your project, understand critical bend radius calculations that many engineers overlook, and gain practical troubleshooting strategies. Whether you're prototyping a new product or planning large-scale production, mastering these fundamentals will help you achieve consistent, high-quality results in your curved aluminum extrusion projects.
Sounds complex? Selecting the right alloy for aluminum bending doesn't have to be overwhelming. The truth is, your choice of alloy determines whether your project succeeds with smooth, crack-free curves—or fails with unsightly fractures. Understanding the differences between common alloys like 6063, 6061, and 5052 gives you a critical advantage before you ever apply force to the material.
Two factors matter most when evaluating alloys for aluminium bending: the alloy series itself and the temper condition. Get both right, and you'll achieve predictable, high-quality results. Get either wrong, and you're inviting problems that no bending technique can fix.
When engineers discuss aluminum bending, the conversation often centers on 6063 and 6061—two popular alloys from the 6XXX series with distinctly different bending characteristics.
6063 aluminum is often called the "architectural alloy" for good reason. According to industry experts at Hydro, 6063 is a good choice for bending applications because of its excellent formability. Its lower strength compared to 6061 translates directly into easier forming with less risk of cracking during the bend.
6061 aluminum offers superior strength but demands more careful handling. For thick pieces of 6061, you'll need bigger bend radii to prevent breaking. When working with tempered 6061-T6, avoid sharp angles entirely. For 0.125-inch thick 6061-T6, use an inside radius that is 1.5 to 3 times the material thickness, and avoid bending past 86 degrees to prevent cracks.
Here's the key insight: if bendability is your priority, lean toward 6063. If you need higher structural strength and can accommodate larger bend radii, 6061 remains viable with proper technique.
Imagine trying to bend a paperclip versus a hardened steel wire—that's essentially the difference between soft and hard tempers in aluminum. The temper designation tells you how the aluminum has been heat-treated or work-hardened, directly impacting how it responds to bending forces.
For 6XXX series heat-treatable alloys, the T4 temper offers lower yield strength and easier bending. However, there's a trade-off: yield strength in T4 condition varies over time due to natural aging, a slow hardening process that can cause springback variation in some bending processes.
The T6 temper, while harder to bend, provides more consistent properties. In some cases, bending in T6 proves more predictable despite requiring more force. Special heat treatments exist that stop natural aging, allowing the material to be heat-treated to T6 after bending—worth considering for critical applications.
Here are the most common tempers for aluminum bending:
When your design demands tighter curves than 6XXX alloys can deliver, 5052 aluminum bending becomes your go-to solution. This alloy from the 5XXX series offers a compelling combination of moderate-to-high strength with superior formability compared to 6061 and 7075.
You'll find 5052 commonly specified for marine equipment and medical devices—applications where both corrosion resistance and tight bends are essential. The alloy bends better than 6061, allowing tighter radii with fewer cracks. If your project involves complex curves or demanding geometries, 5052 deserves serious consideration.
| Alloy Type | Bendability Rating | Recommended Applications | Key Considerations |
|---|---|---|---|
| 3003 | Excellent | Gutters, roofing, storage tanks | High elongation, easy to work with, corrosion resistant |
| 5052 | Very Good | Marine equipment, medical devices, automotive panels | Better bendability than 6061, moderate-to-high strength |
| 6063 | Good | Architectural profiles, window frames, decorative elements | Good choice for general bending, lower strength than 6061 |
| 6061 | Moderate | Structural applications, frames, machinery components | Requires larger bend radii, heat treatment may help |
| 6082 | Difficult | High-strength structural components | More difficult to form, use caution with tight radii |
The general principle holds true across all alloys: minimum bend radius typically equals 1 to 3 times the material thickness, but this ratio increases for harder alloys and tempers. Always check the elongation percentage in material datasheets—alloys with higher elongation bend easier and resist cracking better.
Now that you understand which alloys bend best, you're ready to explore the specific bending methods available and determine which technique matches your project requirements.
When you're ready to transform straight aluminum profiles into curves, choosing the right bending method becomes your next critical decision. Each technique offers distinct advantages—and limitations—that directly impact your project's quality, cost, and timeline. Let's break down the six primary methods used across the industry so you can match the right process to your specific requirements.
Imagine pulling a rubber band while wrapping it around a curved form—that's essentially how stretch bending works. This method places the aluminum extrusion in constant tension while forming it around a bending die, creating smooth curves with minimal distortion or surface damage.
Stretch bending excels when you need:
The trade-off? Tooling costs run higher than most other methods because each project typically requires a custom bending die. However, if you're producing larger volumes using the same profile, those die costs spread across more units, making stretch bending increasingly cost-effective at scale.
These two methods represent the workhorses of aluminum profile bending, but they serve fundamentally different purposes. Understanding when to use each saves time, money, and frustration.
Rotary draw bending clamps your extrusion and pulls it around a rotating die that matches your required radius. According to tube forming specialists, this method delivers highly accurate bends at high speeds with exceptional repeatability. You'll achieve centerline radii as tight as 0.7 times the tube diameter—perfect for aluminum tube bending applications requiring precision.
Choose rotary draw when your project demands:
Roll bending (also called three-roller bending) pushes your profile through a pyramid arrangement of rollers, creating gradual curves. This approach shines for bending long aluminum extrusions and can even form fully circular components.
Roll bending works best for:
The key difference? Rotary draw bends one segment at a time with exceptional precision. Roll bending curves the entire extrusion length but may require multiple passes for tighter radii, which can reduce precision compared to single-operation methods.
When you're working with thin-walled aluminum tubes or hollow profiles, standard bending methods risk collapse or deformation. That's where mandrel bending enters the picture. This technique inserts a solid or segmented support inside the tube during forming, maintaining the profile's shape throughout the bend.
Three mandrel types serve different applications:
Ball mandrels prove particularly valuable for thin-wall aluminum tube bending. Position them precisely at the bend's starting point, then advance in small increments until you achieve a clean result. The gap between mandrel and tube interior stays remarkably tight—approximately 0.009 inches—requiring proper lubrication to prevent galling.
Ram bending (sometimes called push bending) represents one of the simplest and least expensive approaches to bending aluminum. A hydraulic ram pushes the extrusion against pivot blocks or dies, creating the bend through direct force application.
This method suits projects where:
The honest trade-off with ram bending? It's more likely than other methods to deform profiles in undesirable ways since the tube interior lacks support. For structural applications where aesthetics matter less than function—think exhaust systems or industrial frames—this limitation may be perfectly acceptable.
Press bending operates similarly, using two dies pressed against the profile to imprint bend shapes. It's fast and economical but shares ram bending's accuracy limitations and profile deformation risks.
Now that you understand each process, here's a consolidated comparison to guide your decision:
| Method Name | Best Applications | Achievable Radius Range | Profile Compatibility | Relative Cost |
|---|---|---|---|---|
| Stretch Bending | Architectural curves, large structural components | Large radii only | Wide range including complex shapes | High (custom die required) |
| Roll Bending | Long sweeping curves, full circles, prototypes | Medium to large radii | Most profiles; caution with thin walls | Low to medium |
| Rotary Draw | Precision bends, automotive, aerospace components | Tight radii (down to 0.7D) | Round tubes, larger profiles | Medium to high |
| Mandrel Bending | Thin-wall tubes, exhaust systems, exercise equipment | Tight to medium radii | Hollow tubes and profiles | Medium to high |
| Ram Bending | Low-tolerance projects, industrial frames, exhausts | 3-4x tube diameter minimum | Simple profiles; risks deformation | Low |
| Press Bending | High-volume simple bends, basic angles | Limited to gentle curves | Simple profiles only | Low |
Two factors consistently drive method selection beyond application type: how complex your profile is and how thick the walls are.
Profile complexity determines support requirements. Simple solid bars tolerate most methods, while intricate hollow profiles with multiple chambers need internal support to prevent collapse. Asymmetrical profiles may require specialized tooling regardless of which method you choose.
Wall thickness creates clear dividing lines:
The interaction between wall thickness and bend radius follows a critical rule: thinner walls require larger minimum bend radii to avoid wrinkling on the compression side or cracking on the tension side. When both factors push toward challenging territory—thin walls with tight radii—mandrel-supported rotary draw bending typically becomes your only viable option.
Understanding these six methods gives you the framework for making informed decisions. But knowing which method to use is only part of the equation—calculating the correct bend radius for your specific alloy and wall thickness comes next.
Ever calculated a bend radius only to watch your aluminum crack on the shop floor? You're not alone. Many engineers apply generic formulas without accounting for the critical variables that determine whether bent aluminum succeeds or fails. Getting the radius right requires understanding how material thickness, alloy properties, and profile geometry interact—knowledge that separates predictable results from costly scrap.
The bend radius is the distance from the inner surface of your material to the center of the curve. Too tight, and you'll see cracking on the outer tension side or wrinkling on the inner compression side. Too conservative, and you waste material while limiting design possibilities. Let's establish the formulas and guidelines that actually work.
The fundamental relationship between material thickness and minimum bend radius varies significantly based on your alloy and application. For aluminum extrusions, here's what the data tells us:
According to industry fabrication guidelines, a common rule of thumb is 5 to 10 times the wall thickness for simple bends. This means a 3 mm thick extrusion would require a minimum bend radius of 15 to 30 mm to avoid cracking under standard cold bending conditions.
However, this range shifts dramatically based on alloy ductility. Machinery's Handbook guidelines provide more nuanced recommendations:
For bending aluminum flat bar, the formula becomes more straightforward since you're working with a simple rectangular cross-section. Calculate your minimum inside radius as the material thickness multiplied by the appropriate factor for your alloy. For aluminium flat bar in 6063-T5, this typically means 1.5× thickness provides a safe starting point.
Here's a practical example: If you're bending a 1/8-inch (3.2 mm) thick 6061-T6 flat bar, multiply by a factor of 2.5 to get a minimum inside radius of approximately 5/16 inch (8 mm). Attempt anything tighter, and you risk fractures along the outer bend surface.
When you move from flat stock to hollow profiles, the rules change significantly. Hollow and solid profiles behave very differently under bending stress—and ignoring this distinction leads to collapsed tubes and distorted cross-sections.
Solid profiles tolerate bending more uniformly because stress distributes across the entire cross-section. A solid rectangular bent aluminum bar can handle tighter radii than its hollow equivalent because there's no internal void to collapse.
Hollow profiles present three distinct challenges:
For hollow profiles, increase your minimum bend radius beyond standard calculations. As noted in extrusion bending research, if you try to bend with a radius smaller than 5× wall thickness on hollow sections, the wall may wrinkle or split on the inner side and stretch or ovalize on the outer side.
Successful bending requires balancing multiple variables simultaneously. Before specifying any bend, evaluate these five critical factors:
Even with perfect radius calculations, real-world bending introduces variability. Professional bending services typically maintain dimensional tolerances that account for springback, material variation, and process consistency.
Springback—the material's tendency to partially straighten after bending—requires compensation in your tooling or overbending strategy. Harder tempers and larger radii increase springback, sometimes requiring angles 2 to 5 degrees beyond nominal to achieve the target bend after elastic recovery.
For quality control on bent aluminum components, measure these parameters:
When defects appear despite correct radius calculations, they often signal issues with alloy selection, temper mismatch, or process parameters—topics that demand their own troubleshooting approach.
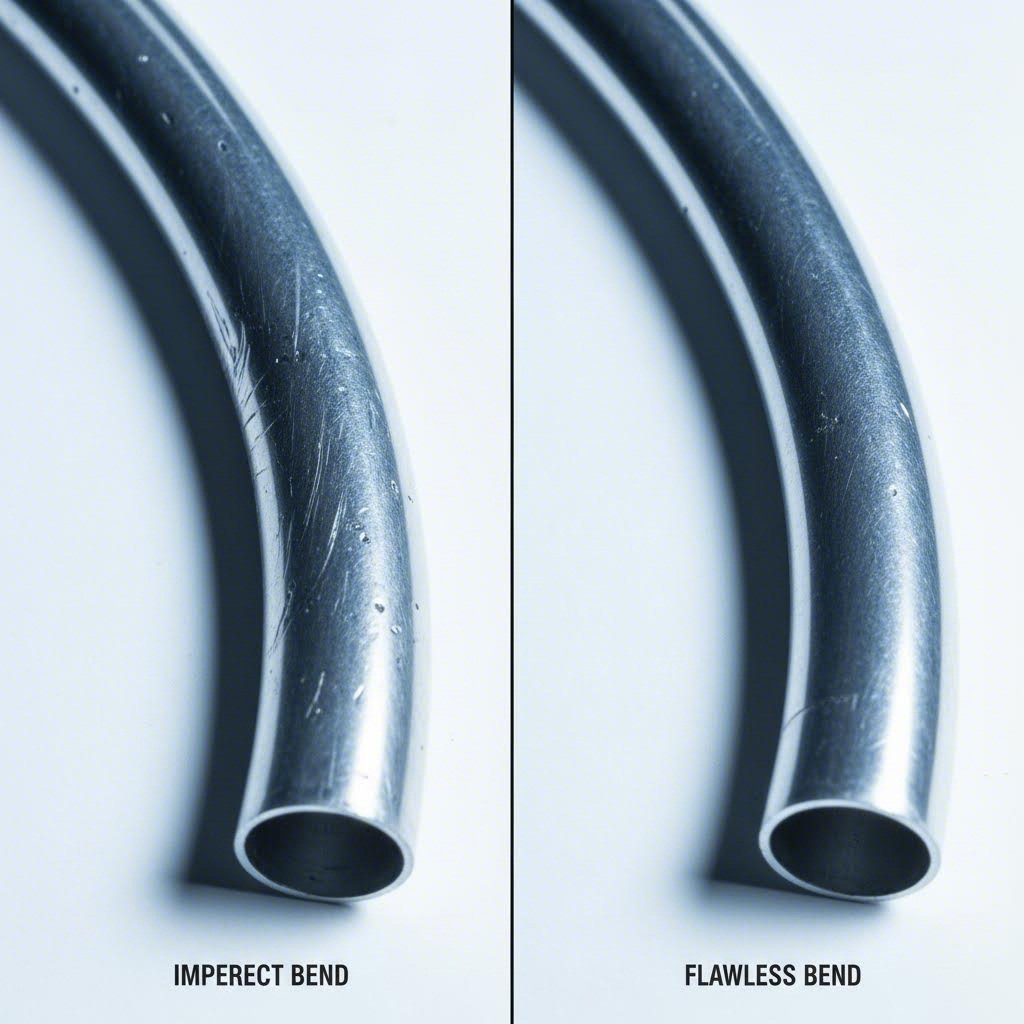
You've selected the right alloy, calculated your bend radius carefully, and chosen an appropriate bending method—yet defects still appear on your curved extruded aluminum. Sound familiar? Even experienced fabricators encounter wrinkling, cracking, and springback. The difference between costly scrap and salvageable parts often comes down to understanding why defects occur and knowing exactly how to prevent them.
Three primary defects plague bending aluminium extrusion operations: wrinkling on the compression side, cracking on the tension side, and springback that throws off your final dimensions. Each has distinct causes and solutions. Let's break them down so you can diagnose problems quickly and implement fixes that work.
When you bend aluminium, the inner radius compresses while the outer radius stretches. If that compression exceeds the material's ability to absorb it uniformly, wrinkles form—rippled distortions that compromise both appearance and structural integrity.
Wrinkling appears most frequently on thin-walled hollow profiles and tight-radius bends. According to aluminum fabrication specialists, softer materials like aluminum are more prone to wrinkling, requiring secure clamping to avoid unnecessary deformation.
For hollow profiles, mandrel insertion proves essential. Position ball mandrels precisely at the bend's starting point and advance incrementally until wrinkles disappear. Wiper dies working in conjunction with mandrels prevent material from buckling inward as it flows around the bend die.
While the inner radius compresses, the outer radius experiences tension—stretching that can exceed the aluminum's ductility limits. When this happens, cracks appear on the outside of your bend, ranging from microscopic fractures to visible splits.
Cracking often signals a fundamental mismatch between your bend radius and material properties. As sheet metal bending experts note, cracking results from the material's hardness and brittleness—materials in harder tempers are prone to cracks if over-bent.
When cracks persist despite radius adjustments, your alloy or temper selection likely needs revision. For applications demanding tight bends, consider bending in a softer condition and heat-treating to final temper afterward—a strategy that preserves formability while achieving required strength.
Springback occurs because aluminum stores elastic energy during bending. Once the tooling releases, that stored energy pushes the metal partially back toward its original shape. According to springback research, aluminum has a relatively high ratio between its elasticity and yield strength, meaning it can return farther than many other metals once the force is removed.
Springback typically ranges from 1 to 5 degrees depending on alloy and hardness—enough to throw off precision assemblies and create fit problems in final applications.
Modern CNC bending equipment addresses springback through adaptive software that calculates required overbending based on material data and past runs. For manual operations, trial-and-error testing on sample pieces establishes the compensation factor before production bending begins.
Beyond technique adjustments, your tooling setup and lubrication practices directly impact defect rates. Proper tooling reduces friction, controls material flow, and provides support exactly where needed.
Key tooling considerations include:
Lubrication prevents galling between mandrels and tube interiors while reducing friction on die surfaces. Apply lubricant uniformly before bending—inconsistent coverage creates localized stress concentrations that trigger defects.
If your finished part requires specific surface treatments, think carefully about timing. Fabrication guidelines recommend bending first and then carrying out surface treatment. Bending after treatments like anodizing or powder coating increases the risk of coating cracking.
When you must bend aluminium extrusion that's already finished, use protective films, increase bend radius beyond standard minimums, and choose flexible coating systems designed to withstand deformation. Even then, expect some surface compromise on tight-radius bends.
Recognizing when defects indicate systemic problems—rather than fixable process issues—saves time and material. Persistent cracking despite larger radii points toward alloy substitution. Uncontrollable wrinkling on complex hollow profiles may require switching to mandrel-supported rotary draw bending. When defects resist all troubleshooting, stepping back to reconsider your fundamental approach often proves more efficient than incremental adjustments.
How do you bend aluminum tubing when you don't have access to industrial equipment? Whether you're prototyping a new design, making repairs in the field, or running small production batches, manual aluminium extrusion bending offers a practical solution—when you understand its capabilities and limitations.
Manual bending works well for specific scenarios, but it's not a universal substitute for professional equipment. Thin-walled aluminum tubing with a diameter less than 3/4 inch can typically be bent by hand with proper technique. Larger diameters, thicker walls, and complex aluminium extrusion types require mechanical assistance or industrial methods to achieve consistent results.
Success with manual bending starts with assembling the right toolkit. Attempting to bend aluminum without proper tools leads to kinking, cracking, and inconsistent angles that waste material and time.
Here's what you'll need for basic manual aluminum tube bending:
For occasional bending projects, a quality handheld tube bender costs far less than outsourcing individual parts. However, the tooling investment only makes sense if you're bending similar sizes repeatedly. According to aluminum tube fabrication specialists, your choice depends on the diameter, wall thickness, and bend radius—a 2-inch aluminum tube bender becomes essential for large-diameter structural tubing.
Ready to make your first bend? Follow this process for consistent results on thin-walled aluminum tubing:
Manual bending serves prototyping, repairs, and small runs well, but recognize where its practical boundaries lie. Professional equipment becomes necessary when:
As aluminum bending specialists note, manual bending offers simplicity and low cost, but it's slow, low precision, and not suitable for large or thick aluminum pieces. For architectural applications or structural components where consistency matters, transitioning to roll bending, rotary draw, or other industrial methods delivers the repeatability that manual approaches cannot match.
Safety deserves final emphasis. Heated aluminum retains temperature longer than it appears, causing severe burns on contact. Always wear heat-resistant gloves when handling recently heated material, and never rush the cooling process—quenching hot aluminum in water can cause thermal shock and microcracking.
Understanding when manual techniques work—and when they don't—helps you make smarter decisions about project execution. For operations that exceed manual capabilities or require consistent high-volume output, the choice between building in-house capacity versus partnering with professional bending services becomes your next consideration.
Should you invest in bending equipment or partner with a professional fabricator? This decision impacts your project costs, timelines, and quality control for years to come. Whether you're bending aluminum extrusions for architectural components, automotive parts, or industrial equipment, understanding the trade-offs between in-house and outsourced operations helps you allocate resources wisely.
The right choice depends on your production volumes, profile complexity, available capital, and long-term growth plans. Let's break down both approaches so you can match your operational strategy to your actual needs.
Bringing bending operations under your own roof offers compelling advantages—but only when your circumstances align with the investment required. According to fabrication industry analysts, businesses choose in-house fabrication to maintain full process control, protect intellectual property, and ensure rapid response to internal production demands.
In-house bending typically makes sense when you:
The challenges? Launching an internal bending operation requires substantial spending on CNC bending machines, tooling sets, facility upgrades, and skilled operators. Many industries also face long-term shortages of qualified technicians—recruiting and training technical staff significantly increases HR costs.
Consider aluminum extrusion CNC equipment as an example: a quality rotary draw bender with computerized controls starts around $50,000 for basic models and exceeds $200,000 for high-precision systems with multi-axis capability. Add tooling for each profile size, maintenance contracts, and operator training, and your true investment climbs considerably higher.
Outsourcing eliminates major capital investments while providing access to specialized expertise you'd struggle to develop internally. Precision tube bending specialists invest heavily in advanced CNC technology, specialized tooling, and operator training—capabilities that would take years to build from scratch.
When evaluating potential bending partners, assess these critical factors:
As aluminum bending service providers emphasize, real-time monitoring and adjustment during CNC bending ensures each bend meets exact specifications. Ask potential partners about their quality assurance checks and whether they provide dimensional reports with finished parts.
Raw cost comparisons often mislead because they ignore volume effects, hidden expenses, and opportunity costs. Use this framework to evaluate your true total cost under each scenario:
| Factor | In-House Operation | Outsourced Partnership |
|---|---|---|
| Initial Investment | $50,000-$250,000+ for equipment, tooling, and training | Zero capital outlay; pay per part or per project |
| Per-Unit Cost (Low Volume: 1-100 parts) | High—equipment amortization spread across few units | Moderate—service fees but no fixed cost absorption |
| Per-Unit Cost (Medium Volume: 100-1,000 parts) | Moderate—breakeven point for many operations | Competitive—volume discounts often available |
| Per-Unit Cost (High Volume: 1,000+ parts) | Low—fixed costs fully absorbed across production | Higher than in-house at scale; margins built into pricing |
| Quality Control | Direct oversight; immediate feedback loop | Dependent on partner capabilities; requires clear specifications |
| Lead Time | Immediate for available capacity | 1-3 weeks typical; expedited options at premium cost |
| Flexibility | Limited by equipment and tooling on hand | Access to diverse equipment without ownership |
| Technical Expertise | Must develop and retain internally | Leverage partner's specialized knowledge |
The crossover point—where in-house costs match outsourcing—varies by project complexity. For simple aluminum profile bending with standard radii, outsourcing often remains cost-effective even at moderate volumes. For complex multi-bend parts requiring specialized tooling, bringing operations in-house pays off faster as volume increases.
Whether you're building internal capacity or selecting a partner, CNC bending technology fundamentally changes what's achievable. Computer-controlled systems eliminate human variability, enabling tolerances that manual operations simply cannot match.
According to CNC bending specialists, advanced software transforms digital designs into tangible three-dimensional aluminum forms with unparalleled accuracy. Automation minimizes the risk of human error, contributing to enhanced overall accuracy in the bending process.
CNC aluminium extrusion bending delivers specific advantages:
When evaluating partners, ask specifically about their CNC capabilities. Modern equipment with real-time monitoring catches deviations immediately, while older machinery may produce acceptable results without the consistency critical applications demand.
Successful outsourcing relationships depend on clear communication. Ambiguous specifications lead to rejected parts, delays, and frustration on both sides. Before submitting your bending requirements, ensure your documentation includes:
Good partners review specifications and ask clarifying questions before quoting. If a potential supplier accepts vague requirements without pushback, consider whether their process controls match your quality expectations.
Making the right choice between in-house and outsourced bending sets the foundation for your project's success. But the decision doesn't end with forming—surface finishing considerations often determine whether you can treat parts before or after bending, adding another layer to your planning process.
Should you anodize before or after bending? What about powder coating? These questions trip up even experienced engineers—and getting the sequence wrong means scrapped parts, coating failures, or compromised aesthetics. The relationship between curved aluminum extrusions and surface treatments requires careful planning that many project specifications overlook entirely.
Surface finishing isn't just a final step—it's a variable that influences your entire bending strategy. Anodized bent aluminum behaves differently than raw mill-finish profiles, and powder coated aluminum bending introduces constraints that affect radius selection. Understanding these interactions helps you design processes that deliver both form and finish without compromise.
The fundamental question—finish before or after bending—depends on your coating type, bend severity, and appearance requirements. Each approach carries distinct trade-offs.
Bending before finishing remains the industry standard for good reason. According to surface finish compatibility research, anodizing usually comes after bending to avoid flaws in the final finish, and powder coating is generally applied after bending to reduce the risk of cracking. When you form raw aluminum first, your coating covers any stress marks left by the process, creating a uniform appearance across the entire profile.
Bending after finishing sometimes becomes necessary when pre-coated material arrives from suppliers or when project timelines don't allow sequential processing. However, this approach demands caution. As pre-anodised aluminum technical guidelines explain, if pre-anodised aluminium is folded, the anodic film of aluminum oxide will crack and crazing will be formed—appearing as fine white lines that may cause a whitening effect in bent zones.
The visibility of this crazing depends on three factors: coating color, viewing distance, and bend radius. Darker colors like bronze or black show crazing more prominently than lighter finishes. Studies on buildings using continuously anodised aluminum over 30 years old show no long-term damage to the surface as a result of bending—the concern is primarily aesthetic, not structural.
Each surface treatment type behaves differently under the stresses of forming. Matching your finish selection to your bending requirements prevents costly surprises.
When circumstances require bending pre-finished material, protective measures become essential. Without proper precautions, tooling contact creates scratches, chips, and marks that ruin the finished appearance.
Effective protection strategies include:
According to technical bending guidelines, the surface must be protected by a protective film to avoid any marks of the folding machine jaws on the surface. This applies equally to anodized and powder-coated materials.
Managing separate vendors for bending and finishing introduces coordination challenges, quality risks, and extended lead times. Parts travel between facilities, specifications must be communicated multiple times, and accountability becomes fragmented when problems arise.
Comprehensive service providers who offer both CNC bending and surface treatments under one roof eliminate these complications. For example, Shengxin Aluminium's deep processing services combine advanced bending capabilities with extensive finishing options including anodizing in custom colors, powder coating, and PVDF treatments. This integrated approach ensures seamless coordination between forming and finishing operations—your specifications flow through a single quality system rather than being interpreted by multiple vendors.
When evaluating integrated providers, verify they offer:
The efficiency gains extend beyond logistics. Integrated providers understand how their bending processes affect subsequent finishing—and vice versa. This knowledge translates into recommendations that optimize both operations rather than each in isolation.
With surface finishing considerations addressed, you're ready to synthesize all these factors—alloy selection, bending method, radius calculations, and finish timing—into a coherent project plan that delivers successful results from the first part to the last.
You've absorbed a wealth of technical knowledge—alloy properties, bending methods, radius formulas, defect prevention, and finishing strategies. Now comes the critical step: translating that knowledge into successful aluminum extrusion project planning. The difference between projects that run smoothly and those that spiral into costly rework often comes down to how well you synthesize these factors before production begins.
Successful custom aluminum bending services don't happen by accident. They result from methodical decision-making that aligns material selection, process choice, and finishing requirements with your specific application demands. Let's consolidate the key frameworks and outline your path forward.
Every bending project presents a unique combination of constraints and requirements. Before committing to any approach, systematically evaluate these four critical factors:
These factors don't exist in isolation—they interact constantly. A tight bend radius requirement may force you toward softer alloys even when strength preferences suggest otherwise. Surface finish demands may dictate process selection regardless of cost considerations. Successful projects balance these trade-offs deliberately rather than discovering conflicts during production.
Ready to move from planning to execution? Follow this practical roadmap to launch your project effectively:
For complex projects requiring precise CNC bending combined with surface treatments, partnering with an integrated provider streamlines execution significantly. Shengxin Aluminium exemplifies this approach—with over 30 years of experience, 35 extrusion presses ranging from 600T to 5500T, and state-of-the-art CNC machining centers, they deliver end-to-end support from die development through mass production. Their comprehensive capabilities including anodizing, powder coating, and PVDF treatments mean your project moves through a single quality system rather than bouncing between disconnected vendors.
Successful aluminum bending projects require more than correct formulas—they demand proper planning, appropriate material selection, and collaboration with experienced fabrication partners who understand how alloy properties, bending methods, and surface treatments interact to deliver quality results.
Whether you're bending architectural profiles, automotive components, or industrial equipment, the principles remain consistent: understand your material, choose methods that match your requirements, calculate radii conservatively, and engage expertise when project complexity exceeds your internal capabilities. Apply these frameworks systematically, and you'll transform bending challenges into predictable, repeatable successes.
Yes, aluminum extrusions can be bent using various methods including stretch bending, roll bending, rotary draw bending, and mandrel bending. The 6000-series alloys like 6063 and 6061 are most commonly used because they offer a good balance of strength and formability. The key to successful bending lies in selecting the right alloy, temper condition, and bending method for your specific profile geometry and required bend radius.
The general rule for bending aluminum is that the minimum bend radius should be 1 to 3 times the material thickness for most alloys, though this increases to 5 to 10 times the wall thickness for hollow extrusions. Softer alloys like 3003 and 6063 allow tighter bends, while harder tempers like T6 require larger radii of 2 to 3 times thickness to prevent cracking. Always check the alloy's elongation percentage—higher elongation means better bendability.
Heating aluminum before bending (annealing) is recommended for harder alloys like 6061-T6 or when attempting tight-radius bends. Heat softens the material temporarily, making it more pliable and reducing crack risk. For manual bending, heat the bend area uniformly until the aluminum becomes workable. However, softer alloys and larger radii often don't require heat, and overheating can permanently weaken the material's structural properties.
The best bending method depends on your application. Rotary draw bending delivers high precision for tight radii and production volumes. Roll bending works best for large-radius curves and full circles. Mandrel bending is essential for thin-walled tubes to prevent collapse. For small-scale work, manual tube benders with internal spring support work well for thin tubing under 3/4 inch diameter.
Alloy 3003 offers the best bendability with minimal cracking risk, making it ideal for gutters and storage tanks. For structural applications requiring better strength, 5052 provides excellent formability with moderate-to-high strength—perfect for marine and medical equipment. Among the popular 6000-series alloys, 6063 bends easier than 6061 due to its lower yield strength, making it the preferred choice for architectural profiles.


 Servicio en línea
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 español
 English
 français
 Deutsch
 русский
 português
 العربية
 ไทย
 Việt
 Українська