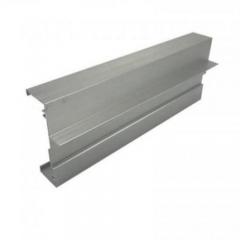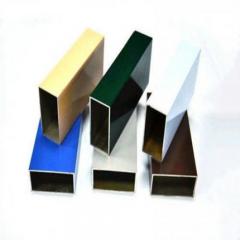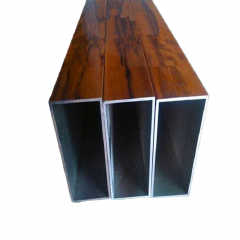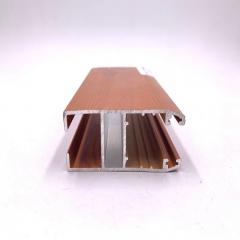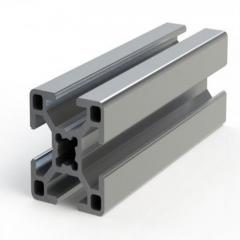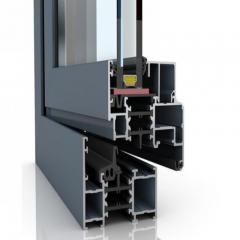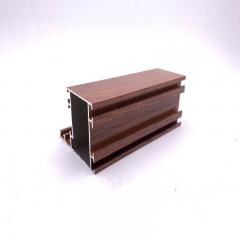
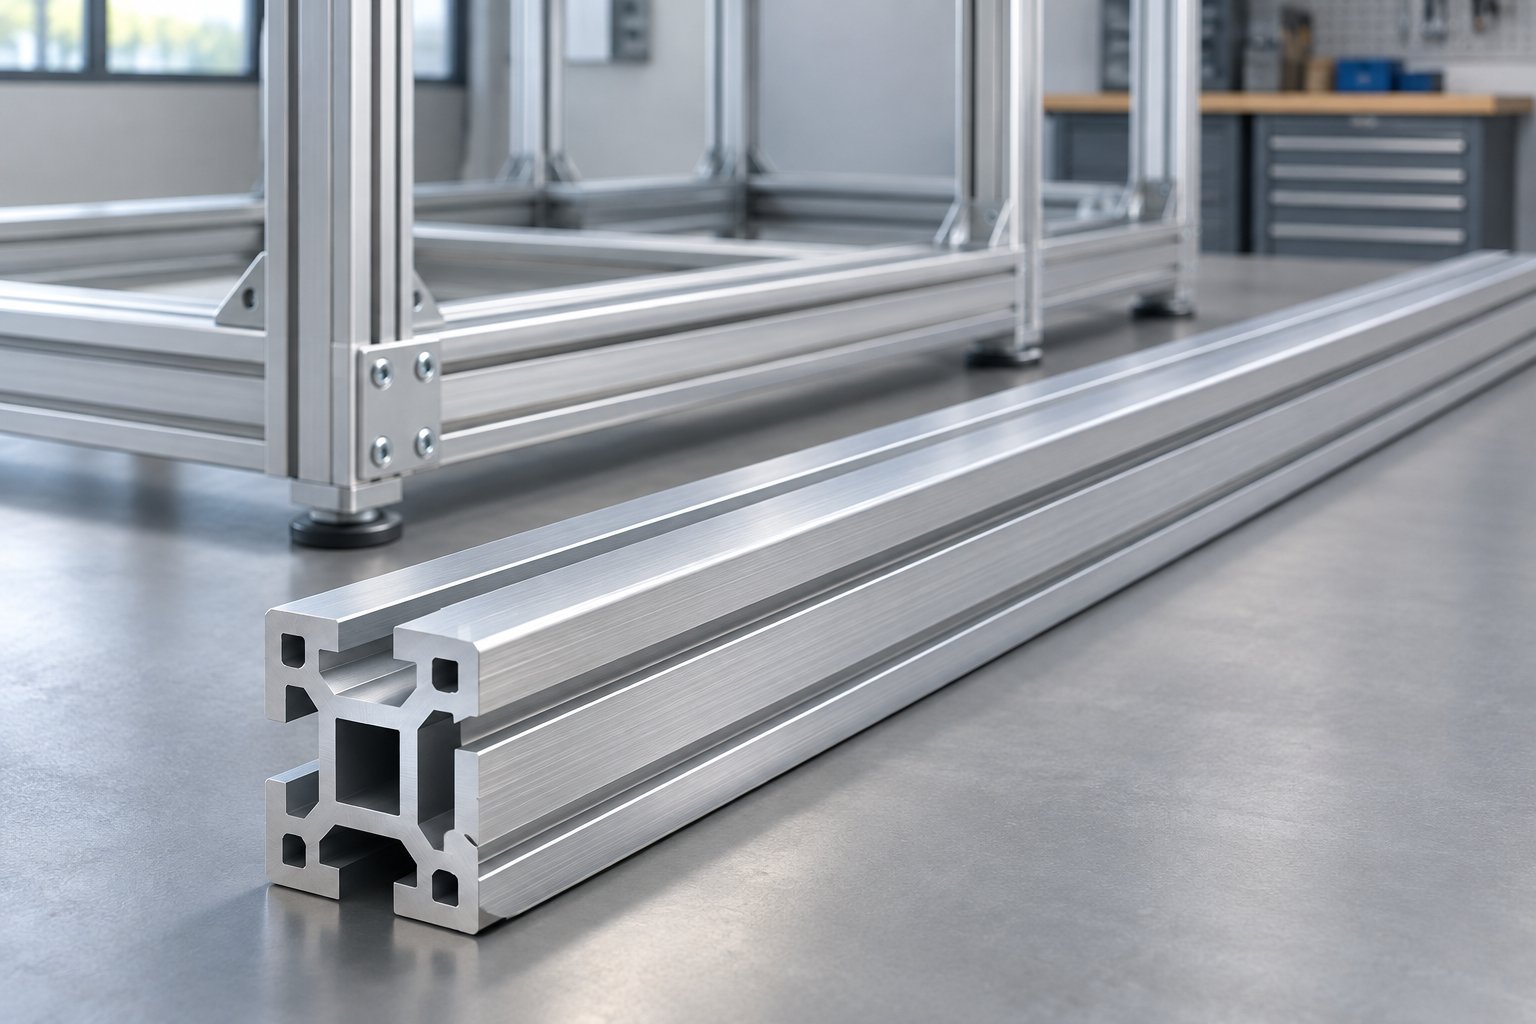
A 4080 aluminium extrusion is a 40 mm x 80 mm rectangular T-slot aluminium profile used to build modular frames, enclosures, and structural assemblies with bolted joints instead of welds.
Have you seen "4080" on a parts list and wondered what the number means? The four digits give the size of the profile. The size also decides how the profile behaves under load, so it matters more than it first appears.
The first two digits give one side of the cross-section in millimeters, and the last two digits give the other side. A 4080 therefore measures 40 mm by 80 mm. Depending on the supplier, you'll see it listed as 40x80, 80x40, or just 40 80. All of these names refer to the same part.
The profile is twice as tall as it is wide. That 2:1 ratio is the main reason to choose it. When the 80 mm side faces the load, the profile resists bending much better than a 40 mm square bar. When the 40 mm side faces the load, most of that advantage disappears. Orientation decides which result you get.
The 4080 belongs to a group of T-slot extrusions that all follow the same naming pattern. A 2020 is 20 mm square, a 2040 is 20 mm by 40 mm, and a 4040 is 40 mm square. Each profile has T-shaped channels running its full length. You slide a T-nut into a channel, and when you tighten the bolt, the nut pulls up against the inner lips of the slot and locks in place. You can attach parts anywhere along the profile, then loosen the bolts later to move or reuse them.
Two other variables matter as much as size:
Two profiles that are both sold as 4080 can differ in series, in alloy, or in both.
Imagine a CNC router gantry that has to stay straight under cutting forces, or a workbench that holds a heavy vise. Builders put a 4080 in places like these, where one member needs extra stiffness in one direction. In industry, T-slot framing is widely used for machine guarding and automation frames. Makers use the same profiles for home builds. Typical uses include:
A factory engineer and a garage hobbyist may order the same 80x40 profile and still need different hardware. The difference comes from the slot.
Say you order a 4080 profile from one shop and a bag of T-nuts from another. Both parcels arrive, and the nuts won't go into the slot. This happens a lot, and the cause is nearly always a series mismatch.
In T-slot framing, a series is a group of profiles that share one slot design. The series number on the label usually tracks the profile size. The width of the slot opening is what decides which T-nuts, bolts, and brackets fit. Two profiles with the same 40 x 80 mm outline can have different slots. Framing Tech, for example, sells 40 series profiles in both 8 mm and 10 mm slot widths and color-codes them so buyers can tell them apart.
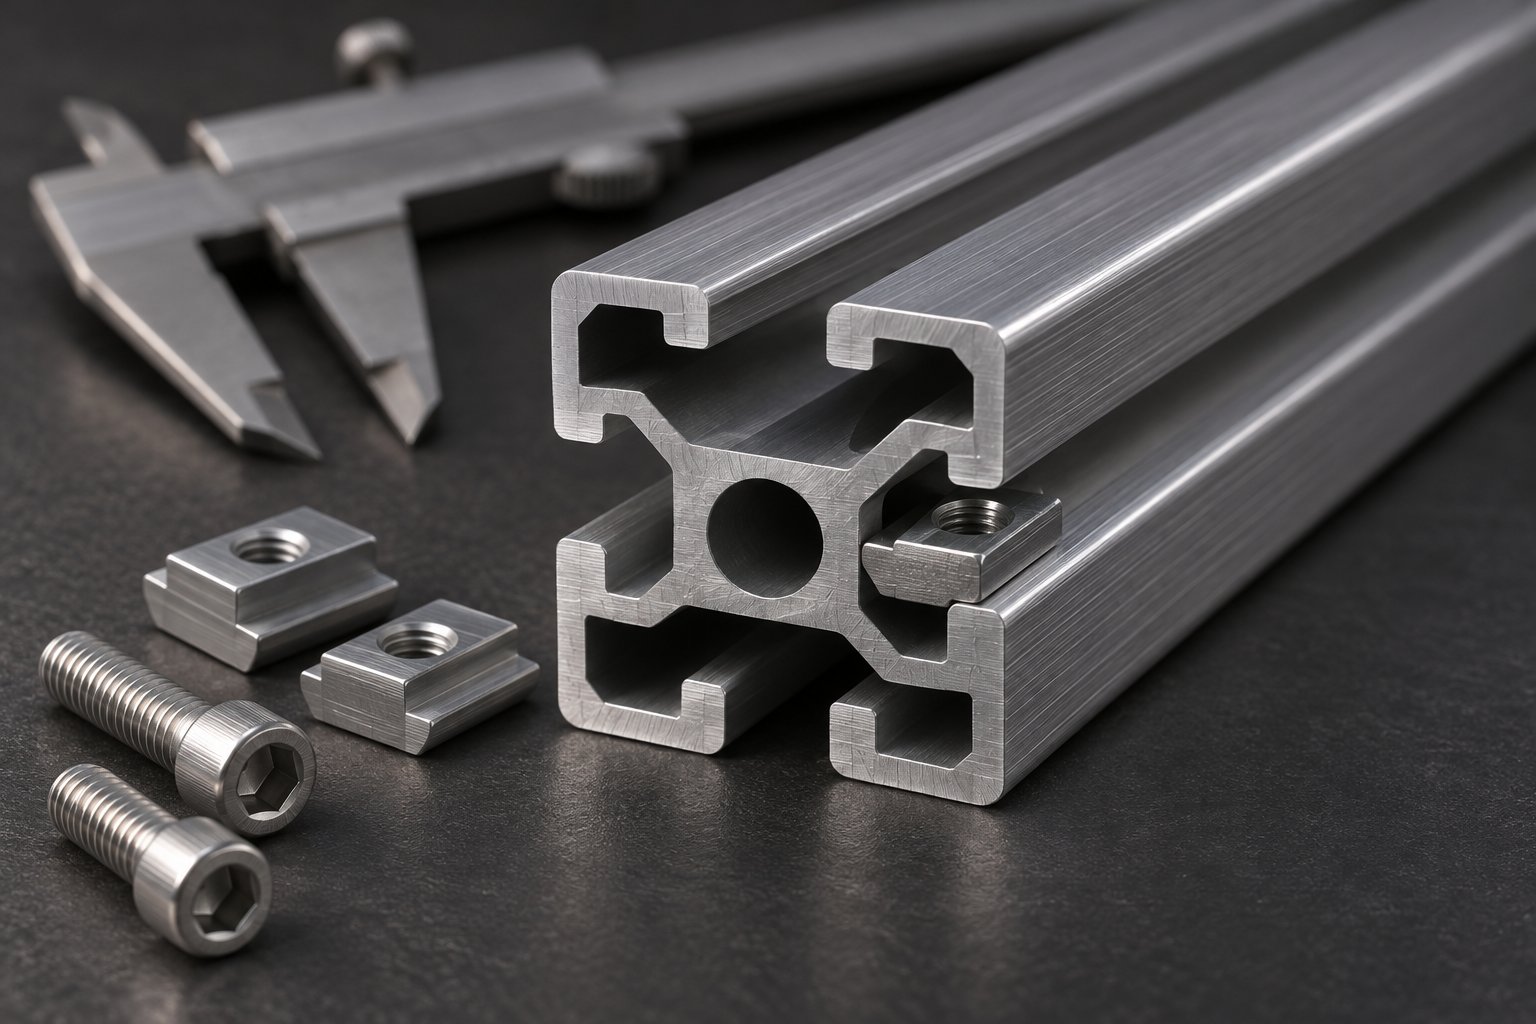
Most metric 4080 profiles use an 8 mm slot and a 6.8 mm center bore, which is the drill size for an M8 tap, as shown in this T-slot size chart. Rectangular profiles use the same slots as the square profiles in their system. A 4080 therefore takes the same fasteners as a 4040 from the same system.
Measure the slot opening with calipers before you order any accessories. These are the common pairings:
The thread size alone won't tell you whether a nut fits. An M8 T-nut made for an 8 mm slot won't hold in a 10 mm slot. Color doesn't change the series either. A clear profile and a black aluminum extrusion from the same system take the same hardware.
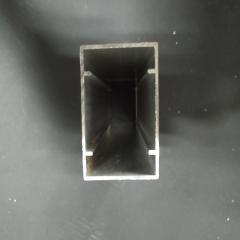
The layout of the slots matters too. A standard 80x40mm profile has six open T-slots: two on each 80 mm face and one on each 40 mm face, as on the 80/20 40-4080. The two slots on each wide face sit 40 mm apart, so brackets drilled for 40 mm profiles line up with them. The profile also has two center bores, one in each 40 mm half. Their diameter matters if you plan to end-tap the profile or use anchor fasteners. Some 4080 variants are lighter or use a different slot arrangement, so check the supplier's end-view drawing before you design around a particular face.
Many people search for "80/20 extrusion" as though it were a generic term. 80/20 is a manufacturer based in Indiana, and its part numbers belong to its own catalog. Its 40-4080 is a metric 40 series profile that takes 40 series fasteners. Profiles from other brands with the same slot width generally accept the same hardware. No universal standard guarantees this, though. A nominal 8 mm slot might measure 8.05 mm from one maker and 7.95 mm from another. That small gap can leave a T-nut loose in one profile and tight in the other. Metric and inch systems never interchange, even when the profiles look alike.
Before you buy hardware in bulk, order a few sample nuts and test them in your actual profile. Calipers will confirm the slot width in seconds. They can't tell you what alloy the profile is made of, and the alloy sets how much load the profile can carry.
Two 40 x 80 profiles can look the same on your bench and still differ in strength. The difference comes from the alloy and the temper, and you'll find both on the material certificate. You can't see either one on the metal.
Most T-slot profiles, the 4080 included, are extruded in 6063-T5. Alloy 6063 flows easily through a die, so it forms the detailed shapes of T-slots and center bores cleanly. It also takes a smooth finish. Because it contains very little copper, it has better corrosion resistance than the other 6xxx alloys.
T5 means the profile is cooled straight from the extrusion press and then artificially aged. T6 adds a separate solution heat treatment and quench before the aging step. T5 skips that step, which keeps processing simpler and avoids one cause of distortion in thin, hollow sections. For enclosures, workbenches, machine guards, and most 3D printer frames, 6063-T5 is strong enough.
Eagle Aluminum lists 6061-T6 at a minimum yield strength of 35,000 psi, compared with 23,000 psi for 6063-T6. For the same alloy, T5 usually reaches lower minimum strength than T6, so the gap between standard 6063-T5 and 6061-T6 is wider than those two figures suggest. Consider 6061-T6 when the frame faces:
6061 has drawbacks. It is harder to push through complex dies, and the extra quench step in the T6 route can twist or bow hollow profiles, which then need straightening. Expect a higher price and often a longer lead time.
If you plan to drill, tap, or CNC-machine your profiles, the alloy also affects how they cut. Kloeckner Metals rates the machinability of 6061 as "good" and 6063 as "fair." The harder 6061 tends to cut cleaner threads, while the softer 6063 is more likely to leave burrs. Temper also changes cutting forces, and a long profile can move after heavy machining on one side.
You can't identify the alloy by looking at it. Write the full designation, such as "6063-T5" or "6061-T6," on the purchase order, and check that the mill certificate shows the same designation. "T6 aluminum" on its own is not a complete specification.
Upgrading the alloy has one limit. Both alloys bend about the same amount under the same load, because their stiffness is almost identical. 6061-T6 raises the load a profile can take before it bends permanently, but it does little to stop a long beam from sagging. To reduce sag, turn the 80 x 40 profile so its deep side lines up with the load.
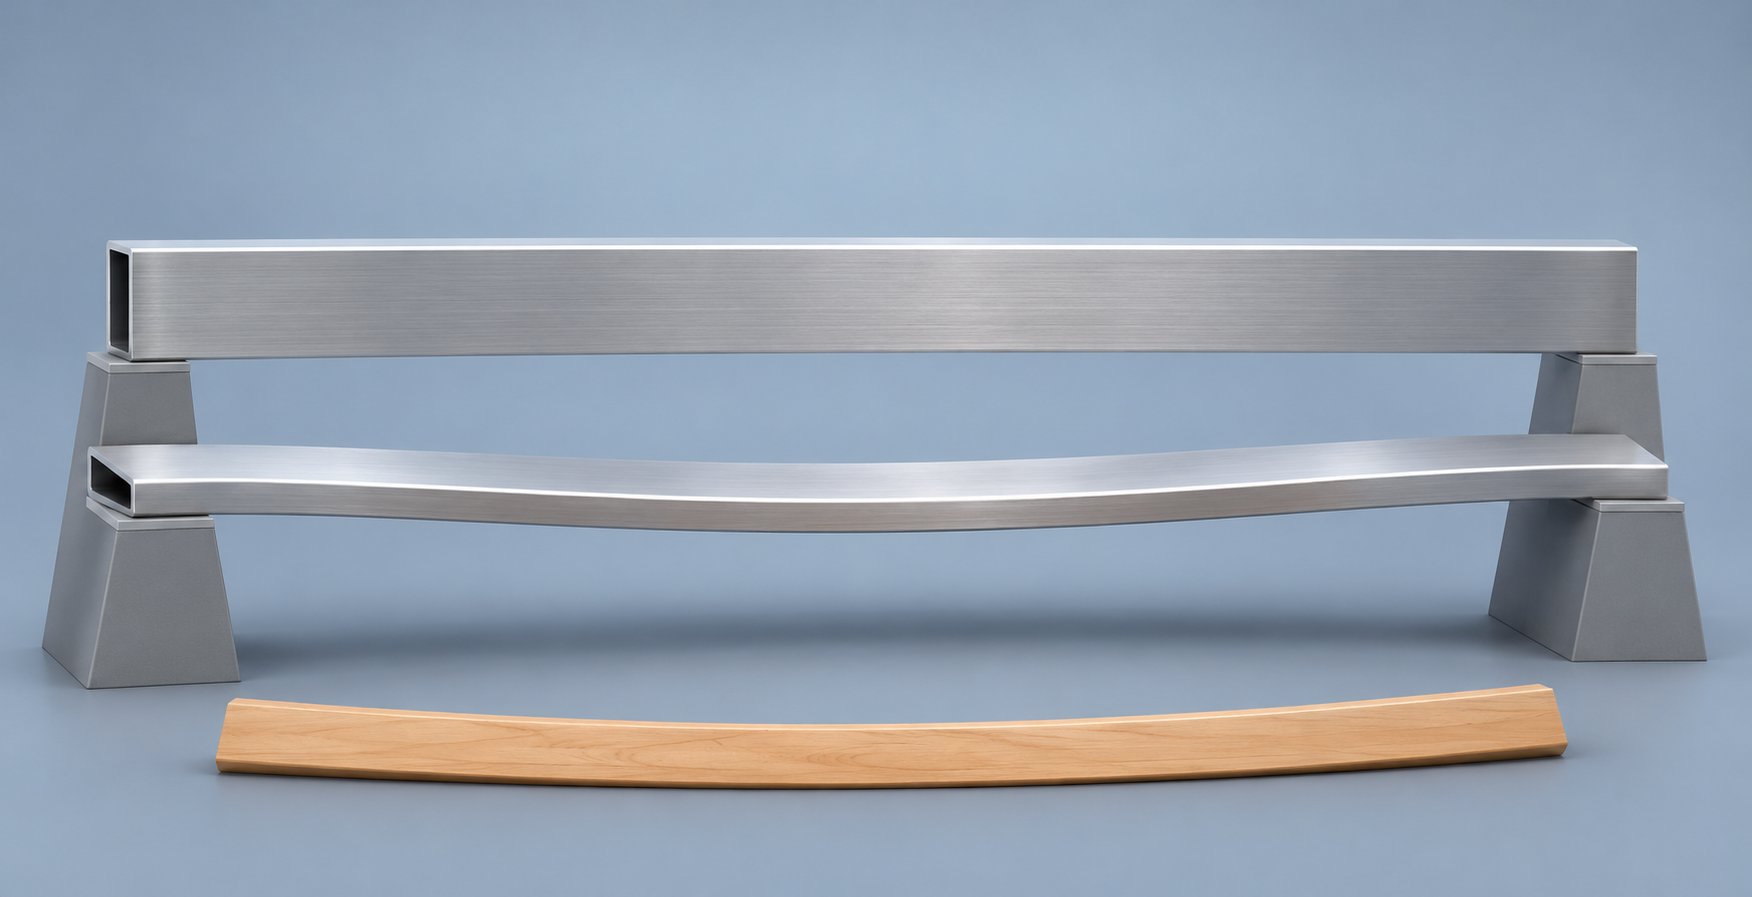
Imagine two identical 4080 beams spanning the same gap and carrying the same weight. One sags visibly, and the other barely moves. The only difference is that someone turned the first beam 90 degrees before bolting it in.
A beam's resistance to bending depends on its area moment of inertia, written as I. This value describes how far the material sits from the center of bending. For a rectangle, the depth measured in the direction of the load is cubed in the formula. Structural software maker RISA points out that doubling a beam's height makes it eight times stiffer, while doubling its width only doubles the stiffness.
Think of a ruler: it flexes easily when you push on its flat face, but it barely bends when you push on its edge, and a 4080 behaves the same way.
When the 80 mm side lines up with the load, the profile bends about its strong axis. Turn it so the 40 mm side faces the load, and it bends about its weak axis. For a 2:1 rectangle, the strong axis is roughly four times stiffer. Vention's datasheet for its 45 x 90 mm profile, a close 2:1 equivalent, lists an Ix of 1,111,757 mm4 and an Iy of 287,967 mm4, a ratio of about 3.9. Bending strength depends on I divided by the distance to the outer edge, so it comes out about twice as high on the strong axis.
Directional stiffness is the main reason to choose a 4080. So what is a 4040 good for? A 4040 is a 40 mm square profile with the same stiffness in both directions, which suits members loaded from more than one side. A 4080 adds a lot of stiffness in one direction without the weight and cost of an 8080. Vention's figures show the trade-off: its 45 x 90 profile has about 6.8 times the strong-axis stiffness of its 45 x 45 profile at about 1.6 times the weight per meter.
The drawing may label the part 80 x40 or 40/80, but the values to check are the manufacturer's published Ix and Iy for your exact profile variant. Light-duty versions and different slot layouts change the internal geometry. Manufacturers also differ on which axis they call Ix, so confirm the orientation on the datasheet drawing. Datasheet values also show whether a 4080 is the right size for the job, or whether a 2040, 4040, or 8080 would suit the span better.
When you plan a frame, the choice usually comes down to four sizes. Which one goes where? The answer depends on how much stiffness each size gives you for its weight.
The stiffness figures for the 4080 and 4040 come from PB Aluminum profile data for 8 mm slot profiles. The weight ranges come from a T-slot size chart and vary from one manufacturer to the next.
| Profile | Cross-Section (mm) | Approx. Weight (kg/m) | T-Slots | Relative Strong-Axis Stiffness | Best-Fit Uses |
|---|---|---|---|---|---|
| 4080 | 40 x 80 | 2.4 to 3.2 | 6 | About 7x a standard 4040 (I = 73.7 vs 9.9 cm4). The weak axis is still about 2x a 4040 (19.1 cm4). | Gantry beams, long horizontal spans, machine base rails |
| 2040 | 20 x 40 | 0.85 to 1.00 | 6 | Well below a 4040, even on its strong axis | Light frames, 3D printer frames, panel support |
| 4040 | 40 x 40 | 1.45 to 1.70 | 4 | Baseline, the same in both axes | Columns and members loaded from several directions |
| 8080 | 80 x 80 | Roughly double a 4080 | 8 on most versions | Roughly double the 4080's strong axis, in both directions | Heavy machine bases, large CNC gantries |
The stiffness ratios for the 2040 and 8080 are estimates based on geometry. Check the datasheet for the exact profile you plan to buy.
The 4080 weighs less than twice as much as a 4040 but is about seven times stiffer when the 80 mm side faces the load. The 2040 is lighter and cheaper, and it flexes much more. The 4040 (sold by 80/20 as the 40-4040) bends the same amount in either direction, but it is less stiff in both directions than a 4080 on its strong axis. The 8080 is the heavy-duty choice, and its price usually tracks its weight.
The 2080 also deserves a mention. This 20 x 80 mm profile is deep but narrow. It resists vertical loads well but bends and twists easily sideways. It fits where width is limited, such as tall panel edges, as long as bracing holds it straight. Most 2080 profiles use 20 series slots, so they take smaller hardware than a 4080.
Compare profiles by their Ix and Iy values. Cross-section area or weight can mislead you. For a beam loaded at its center, deflection equals PL3/(48EI). Suppose a 500 N load (about 51 kg) sits at the middle of a 1,000 mm span. A standard 4040 sags about 1.5 mm. A 4080 on its strong axis sags about 0.2 mm. If your machine needs an L/1000 limit, which is 1 mm on this span, only the 4080 passes. Double the span to 2,000 mm and the 4080's sag grows eightfold to about 1.6 mm. That still meets the 2 mm limit for that span. These figures leave out the beam's own weight, so treat them as a starting point. Span length, applied load, and deflection limit should drive the choice. Price comes after those.
Many frames use several sizes. A typical layout puts 4080 on the main beams and 2040 or 2020 on bracing and panel supports. MISUMI points out that lightweight profiles on non-critical members can reduce cost and weight across a large build. Smaller sizes have a hardware cost of their own, though. A 2020 uses a 6 mm slot and a 4080 usually uses an 8 mm slot, so you need two sets of T-nuts and two parts bins, and assembly mistakes become more likely. To keep a single series, some builders use 4040 for the secondary members instead.
The datasheet shows the same stiffness for a raw profile and a black aluminium extrusion, and the finish does not change how much the beam bends. The finish does affect how easily T-nuts slide into the slot.
Can the finish change how your frame goes together? Yes. The finish coats every surface of the profile, and that includes the inside of the T-slots where the nuts slide. The trade-offs below apply to every size, from a slim 2080 aluminum extrusion to a heavy 8080 extrusion.
Mill finish is the bare profile as it comes off the press. It costs the least and suits members hidden inside a machine base. It picks up fingerprints, slowly forms a dull oxide, and can look different from one length to the next.
Clear anodizing is the usual finish on T-slot framing. This electrochemical process grows an oxide layer out of the aluminum itself, so the layer won't flake or peel. Protolabs gives a 10 micron minimum average thickness for clear Type II anodizing. A layer that thin has little effect on how T-nuts fit, and it makes the surface much more resistant to scratches and corrosion.
You'll see black anodized profiles on many CNC machines, 3D printer enclosures, and display frames. Dyed finishes need a thicker layer. Protolabs sets a 15 micron minimum average for black and colored anodizing. The layer forms on both walls of the slot, so a slot already at the narrow end of its tolerance can feel tight. Before final assembly, slide a T-nut and a bracket along each profile to check that they move freely. Anodized color can vary slightly from batch to batch, so order all the visible lengths at the same time.
Powder coating sprays a charged powder onto the metal, and heat cures it into a film 50 to 150 microns thick. It comes in almost any RAL color, and outdoor-rated powders hold up well in sun and weather. A film that thick on both walls of an 8 mm slot can narrow the opening by 0.1 to 0.3 mm, which is enough to block a T-nut. Protolabs recommends masking tight-fit areas before coating. If the coating chips, the bare metal underneath is exposed to corrosion. The film also starts to break down above 200 degrees C.
Plan your electrical grounding as well. Anodized and powder-coated surfaces don't conduct electricity. If you bolt a ground lug to a coated face, it may never touch bare metal, whether on a 4080 router gantry or on an 8080 aluminum extrusion base that carries a spindle drive. Leave a raw or lightly sanded spot at each grounding point, then confirm continuity with a multimeter.
Drilling after finishing exposes raw aluminum in the hole. This means the way you plan to join the profiles also decides whether machining should happen before or after the finish goes on.
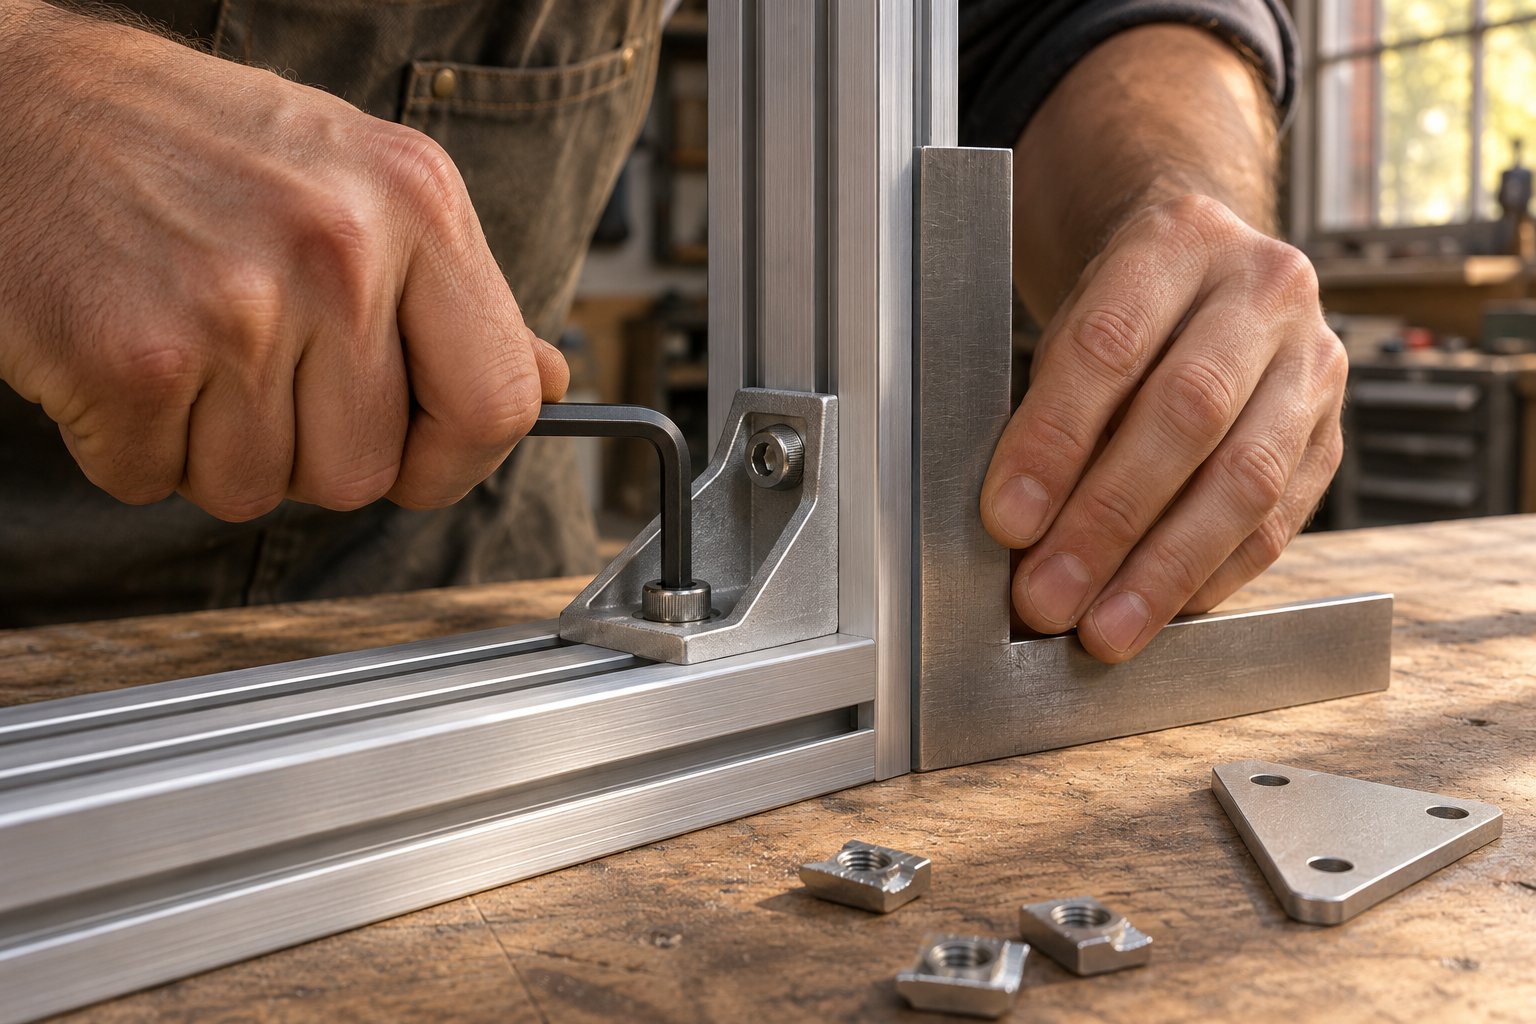
Where will each joint go, and how will you fasten it? Decide that before the profiles get their finish. A hole drilled after anodizing leaves raw aluminum exposed, and holes drilled on site are easy to put in the wrong place. T-slot frames use four main types of connection. Here they are from simplest to most demanding:
Brackets work well on enclosures, shelves, and any joint where the load is modest or the layout may change. A single bracket has one weakness: a sideways force can twist the joint around it. Tall uprights and cantilevered arms therefore need a bracket on each side or a gusset plate. The gussets in Framing Tech's connector guide have a removable alignment tab that sits in the slot and stops the gusset from rotating. Their slotted holes allow small position adjustments. Each 80 mm face of a 4080 has two slots 40 mm apart, so brackets made for any 40mm aluminum extrusion in the same series will fit. For a stiffer joint, pick a plate wide enough to bolt into both slots.
Blind joints look clean, so builders often use them on machine bases and display frames. One common type uses a connection screw. You tap the end of one profile, thread the screw in, and slide its head into the slot of the crossing profile. You then tighten the screw with a hex key through a small access hole drilled in that profile. Anchor-style universal fasteners work in a similar way. You first set the fastener head loosely in the slot of the adjacent profile. The body then seats in a counterbore machined into the base profile. Tightening the set screw pulls the two profiles together and stops the joint from rotating.
The end of a 4080 has two center bores. If you tap both and use two fasteners, the joint can't pivot. An M8 tap is the usual choice for the standard 6.8 mm bore. Shengxin's assembly guide recommends thread engagement of at least 1.5 times the bolt diameter, which works out to 12 mm for M8. Each access hole has to line up with the bore and the slot. If it doesn't, the screw head binds before the joint pulls tight.
Whether your drawing calls the part a 4080 or an 8040 aluminum extrusion, a supplier with CNC equipment can cut, drill, and end-tap each length to your drawing. Shengxin Aluminium, for example, lists CNC machining support for its 40 x 80 mm T-slot profile, so the lengths for blind joints can arrive ready to assemble. Ask the supplier whether machining happens before or after finishing, because the order decides whether the holes end up protected. The same listing offers 6063-T5 and 6061-T6. For threaded joints that carry vibration or heavy loads, 6061-T6 gives stronger threads that also cut more cleanly. For light frames, 6063-T5 is strong enough.
Each of these tips prevents a specific error. Builders keep running into the same small set of problems, and many of those problems start on the order form, long before the first bolt goes in.
Have you ever finished a frame and then found that one part doesn't fit or one beam sags? Most of these problems come from choices made earlier, while picking parts from a catalog or filling in the order. Builders run into the same five mistakes again and again:
The product name won't tell you the slot width. Suppliers list the same part as 4080 extruded aluminum, 40x80, or 8040 aluminum extrusions, and none of those names includes the slot size. Shengxin's guide to profile naming warns that the same four digits can mean an inch profile in one catalog and a metric profile in another, and that hardware is chosen by series rather than outside size. JLCMC also advises builders to measure the groove width so a T-nut slides without binding or play. A 4080 and an 80/20 40-4040 profile belong to the same series and take the same hardware. An inch-based 15 series profile of similar size does not.
Under a center load, sag grows with the cube of the span. A 4080 that sags 0.2 mm over 1,000 mm will sag about 1.6 mm over 2,000 mm. Under an evenly spread load, such as a shelf full of parts, sag grows with the fourth power of the span, using 5wL4/(384EI). For both 6063 and 6061, E is about 69,000 N/mm2. On a long gantry, add the profile's own weight to the load. If the result comes close to your limit, add a support at mid-span or move up to a larger profile.
A quick sketch prevents most of these errors. Draw the frame, mark every connection point, and note what each slot needs to hold. Choose the hardware series before you order any parts. Slide-in T-nuts have to go in before assembly. Drop-in nuts can be added later, but panels can't be added once a slot is closed. Last, check the alloy on the purchase documents before you approve the order.
Once the frame is planned to this level, you have a clear list of requirements to send a supplier. Next you need to decide who should fill it: a distributor that stocks standard lengths, or a manufacturer that cuts, machines, and certifies each part to your drawing.
Your sketch is done, your cut list is written, and you know which alloy you need. The next decision is who makes the parts. That depends on how many lengths you need, how much machining each one needs, and how soon you need them.
A distributor keeps standard profiles in stock and ships them fast. You can order a few pieces, often cut to length, so distributors suit prototypes, repairs, and one-off builds. You usually choose from the finishes and machining options the distributor already offers.
An OEM manufacturer runs its own extrusion presses. It can supply custom lengths, your choice of alloy and finish, and parts drilled and tapped to your drawing. In return, you accept a minimum order and a production lead time. Shengxin Aluminium's 40 x 80 mm T-slot profile shows what this looks like in practice. The listing offers 6063-T5 or 6061-T6, 5.8 m or custom lengths, finishes from mill and anodized to powder coated, and CNC cutting, drilling, and tapping. Its minimum order is 500 kg. At the 2.4 to 3.2 kg/m weights listed earlier, that comes to roughly 155 to 210 meters of 4080 aluminum, which gives you a sense of where OEM pricing starts.
Bor USA advises buyers to compare total cost rather than price per kilogram. A cheap profile that arrives out of tolerance or needs extra machining ends up costing more. Before you approve a supplier, check these points:
Ask for a sample or a short test piece before you commit to a production run. Shengxin lists free samples, though the buyer pays freight. Fit your T-nuts, brackets, and anchor fasteners to the sample, and inspect the finish on any face that will be visible.
For a single 3D printer enclosure, a distributor and a pair of calipers are all you need. For a run of fifty machine bases with blind joints, a manufacturer that machines every length to your drawing is the better fit. Many projects use both: a distributor supplies the prototype, and an OEM takes over for production once the design is final.
Whichever supplier you choose, the 40 x 80 mm outline does not tell you the load capacity, the slot fit, or the joint strength. Two parts both listed as 40x 80 can differ in wall thickness, slot width, or bore size, and 4040 aluminum extrusion dimensions vary between catalogs in the same way. Confirm these values for your exact profile and joints, using the supplier's datasheet and a test piece, before you order the full frame.
The number gives the outside size of the cross-section: 40 mm on one side and 80 mm on the other. That makes the profile a 2:1 rectangle. Catalogs may list the same part as 40x80, 80x40, or 8040, and the order of the digits doesn't mean a different product. The name leaves out several things that matter just as much. It doesn't tell you the slot width (the series), the alloy and temper, the wall thickness, or whether the profile is a light-duty variant. Two parts both sold as 4080 can take different T-nuts and carry different loads. Check the supplier's end-view drawing and datasheet before you design around one.
Yes, as long as you mount it the right way. Bending stiffness depends on the profile's moment of inertia, and the depth in the direction of the load counts most. PB Aluminum figures for 8 mm slot profiles show that a 4080 with its 80 mm side facing the load is about seven times stiffer than a standard 4040. Turned on its flat side, it is still about twice as stiff. It weighs less than twice as much as a 4040. In practice, a 500 N center load that bends a 4040 about 1.5 mm over a one-meter span bends a correctly oriented 4080 only about 0.2 mm. For gantry beams and shelf rails, stand the 80 mm side upright. For columns, point the 80 mm side toward the main sideways force and brace the 40 mm direction against buckling.
Hardware fit depends on the slot width, so start there. Most metric 4080 profiles have an 8 mm slot, which takes 8 mm T-nuts with M6 or M8 bolts. Some 40 series profiles use a 10 mm slot instead, which needs 10 mm T-nuts with M8 bolts. Inch-based profiles of similar size use different hardware and never mix with metric parts. The standard 6.8 mm center bores can be tapped M8 for end connections. Nominal slot widths can differ by a few hundredths of a millimeter between brands. Measure the slot with calipers and test a few sample nuts before you buy hardware in bulk. The finish matters too: black anodizing and powder coating add thickness inside the slot and can make nuts slide tightly.
6063-T5 is the standard choice and is strong enough for enclosures, workbenches, machine guards, and most 3D printer frames. Choose 6061-T6 when the frame sees repeated start-stop motion, vibration from spindles or motors, or loads that people work beneath. Eagle Aluminum lists 6061-T6 at a minimum yield strength of 35,000 psi, against 23,000 psi for 6063-T6, and 6063-T5 sits lower still. 6061-T6 also cuts cleaner threads for blind joints, but it costs more and often takes longer to produce. Upgrading the alloy has one limit: both alloys have nearly the same stiffness, so 6061-T6 won't stop a long beam from sagging. Orientation and profile size control sag. Whichever alloy you pick, write the full alloy and temper on the purchase order and confirm it on the mill certificate.
For a few pieces, a distributor is the fastest option, because it stocks standard profiles and can often cut them to length. For production runs that need custom lengths, a chosen finish, and pre-drilled or tapped ends, an OEM manufacturer fits better. Shengxin Aluminium's 40 x 80 mm T-slot framing profile is one example. It offers 6063-T5 or 6061-T6, customizable lengths, several finishes, and CNC machining support, with a 500 kg minimum order. Depending on profile weight, that is roughly 155 to 210 meters. Before you order from any supplier, ask for a datasheet with Ix and Iy values, a mill certificate, and a sample piece. The 40 x 80 mm size alone doesn't define load capacity, slot compatibility, or connection design, so confirm them for your actual assembly.


 Servicio en línea
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 español
 English
 français
 Deutsch
 русский
 português
 العربية
 ไทย
 Việt
 Українська